
A CNC-machined surface can look perfectly flat and still be unsuitable for a mechanical seal, optical assembly, precision valve, gauge component, or semiconductor fixture.
The reason is simple: surface finish and flatness are not the same thing.
A surface may have a very low Ra value but still contain:
- Slight bow
- Local high spots
- Waviness
- Thickness variation
- Poor parallelism
- Grinding marks
- Distortion from heat treatment
When these errors begin to affect sealing, alignment, contact, leakage, optical performance, or assembly accuracy, conventional milling or surface grinding may no longer be enough.
This is where precision lapping is used.
Lapping is a controlled abrasive finishing process designed to remove very small amounts of material while improving surface geometry and finish. It is particularly valuable when a component requires extremely flat mating surfaces, controlled thickness, close parallelism, or a very fine surface condition.
Typical applications include:
- Mechanical seals
- Valve plates
- Gauge components
- Precision spacers
- Optical components
- Semiconductor equipment parts
- Pump components
- Ceramic components
- Precision machine components
- Aerospace and medical parts
For many custom precision parts, lapping is not the main machining process. It is the final operation that brings a critical surface from machined accurately to functionally precise.
What Is Precision Lapping?
Precision lapping is a fine abrasive machining process in which a workpiece moves against a lapping plate while abrasive particles remove microscopic amounts of material from the surface.
Unlike milling or turning, lapping does not use a defined cutting edge.
Instead, material removal is produced by many small abrasive particles acting between the workpiece and the lap surface.
Typical abrasives include:
- Aluminum oxide
- Silicon carbide
- Diamond
The abrasive may be suspended in a liquid slurry or used in another controlled lapping system depending on the material and process.
The primary objective is usually not high material removal.
Instead, high precision lapping is used to improve characteristics such as:
- Flatness
- Parallelism
- Thickness
- Surface roughness
- Surface uniformity
- Contact condition
This distinction is important.
If a component needs 1 mm of material removed, lapping is probably not the correct first process.
If a component is already very close to final dimensions but the last few microns determine whether it seals, aligns, or functions correctly, lapping may be exactly the right process.
How Does the Lapping Process Work?
In a typical flat lapping operation, parts are placed against a rotating lapping plate.
Abrasive particles are distributed across the plate, usually through a slurry or controlled abrasive system.
Relative motion between the part, abrasive, and lapping plate gradually removes microscopic high points from the component surface.
The basic process can be summarized as:
Pre-machining → Pre-grinding if required → Lapping → Cleaning → Inspection
The exact sequence depends on the part.
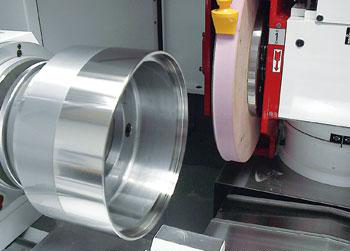
1. Pre-Machining
The component is first manufactured close to final size.
This may involve:
- CNC milling
- CNC turning
- Surface grinding
- Cylindrical grinding
- EDM
- Heat treatment
Lapping should generally not be used to correct large machining errors economically.
Good incoming geometry makes the lapping process faster and more predictable.
2. Preparing the Lapping Plate
The condition of the lapping plate is critical.
The plate must maintain the required geometry because its shape influences the surface produced on the workpiece.
For high-precision flat lapping, plate condition is continuously monitored and corrected.
A plate that becomes excessively concave or convex can transfer corresponding form errors into the parts being processed.
For this reason, plate conditioning is a central part of precision lapping rather than routine machine maintenance.
3. Applying the Abrasive
Abrasive particles are introduced between the component and lapping surface.
The correct abrasive depends on:
- Workpiece material
- Hardness
- Initial surface condition
- Required stock removal
- Required surface finish
- Desired processing time
Coarser abrasive can increase removal rate.
Finer abrasive is normally used when approaching the final surface condition.
4. Controlled Relative Motion
The lapping plate rotates while the components move across its surface.
The goal is to distribute wear evenly across both the components and the lap plate.
Controlled motion prevents the part from repeatedly following the same path.
This is important for both surface uniformity and plate flatness.
5. Progressive Material Removal
The abrasive gradually removes microscopic peaks and high areas.
Compared with conventional machining, the material-removal rate is low.
This is deliberate.
The slow, controlled nature of the process allows geometry to be refined without introducing the relatively large cutting forces associated with heavy machining.
6. Cleaning
Lapping compounds and abrasive residue must be removed thoroughly.
This is particularly important for:
- Hydraulic components
- Medical parts
- Optical assemblies
- Semiconductor equipment
- Precision bearings
- Sealing components
Residual abrasive can damage a precision assembly if it remains on the finished part.
7. Inspection
Finished parts may be checked for:
- Flatness
- Thickness
- Parallelism
- Surface roughness
- Dimensional accuracy
- Cosmetic condition
The inspection method should match the requirement on the engineering drawing.
Why Is Lapping Used?
Precision machining processes can already achieve very good accuracy.
So why add another finishing operation?
Because some applications depend on surface characteristics that cannot be described by a normal dimensional tolerance alone.
Consider two metal plates.
Both are machined to:
10.00 ±0.01 mm thickness
Both parts may satisfy that dimension.
But one may have:
- 8 μm flatness error
while the other has:
- 1 μm flatness error
For an ordinary bracket, this difference may be irrelevant.
For a sealing plate or optical mount, it may determine whether the assembly works.
Lapping is used when these subtle geometric errors become functional requirements.
What Does Precision Lapping Improve?
Precision lapping can improve several surface characteristics simultaneously.
Flatness
Flatness controls how much a surface deviates from a theoretically perfect plane.
This is one of the main reasons for specifying flat lapping.
Applications where flatness matters include:
- Mechanical seals
- Valve plates
- Optical mounts
- Gauge blocks
- Vacuum components
- Semiconductor fixtures
- Precision assembly surfaces
The condition and flatness of the lapping plate directly affect the flatness that can be produced on the workpiece.
Parallelism
A component may require its two opposing faces to remain closely parallel.
This matters when the part controls:
- Assembly height
- Bearing preload
- Spacing
- Alignment
- Compression
- Optical path position
Double-sided lapping can be particularly useful when thickness and parallelism must be controlled together.
Thickness
Lapping removes only a small amount of material, but this can be useful for bringing precision components to tightly controlled final thickness.
Typical examples include:
- Spacers
- Washers
- Valve plates
- Ceramic substrates
- Precision shims
Surface Finish
Lapping can produce very fine surface finishes because material is removed through extremely small abrasive interactions rather than a conventional cutting edge.
However, extremely low surface roughness should not automatically be specified unless the function requires it.
A functional sealing surface, optical component, and precision locating face may each need different surface characteristics.
Surface Contact
Two apparently flat machined surfaces actually contact each other at microscopic high points.
Lapping can increase the effective contact area by reducing these local peaks and improving overall surface geometry.
This can be important for:
- Sealing
- Vacuum systems
- Precision mating surfaces
- Mechanical reference surfaces
Flatness Is Not the Same as Surface Roughness
This is one of the most important concepts in precision finishing.
Surface roughness describes relatively small-scale texture.
Flatness describes the overall form of the surface.
A component can have:
Ra 0.1 μm
and still not be sufficiently flat.
Likewise, a very flat surface may still have a rough texture.
These characteristics should therefore be specified independently when both are functionally important.
A drawing that only says:
Ra 0.2 μm
does not automatically require exceptional flatness.
And a drawing specifying:
Flatness 0.003 mm
does not automatically specify an optical-quality surface finish.
Flat Lapping
Flat lapping is one of the most common forms of precision lapping.
It is used when one or more planar surfaces require greater flatness or surface quality than conventional machining can economically achieve.
Components are placed against a controlled flat lapping plate while abrasive removes small amounts of material.
Flat lapping is commonly used for:
- Seal faces
- Valve plates
- Spacers
- Pump components
- Precision washers
- Carbide components
- Ceramics
- Optical substrates
- Semiconductor components
The process can be performed as either single-sided or double-sided lapping.
Single-Sided Lapping
In single-sided lapping, one primary surface of the component is processed against a lap plate.
It is useful when:
- Only one face is critical
- The opposite side has different geometry
- Part thickness does not require simultaneous control
- The workpiece cannot be processed between two plates
Single-sided systems are widely used for precision flat finishing.
Double-Sided Lapping
Double-sided lapping processes two opposing surfaces simultaneously.
Parts are typically contained within carriers positioned between upper and lower lapping plates.
This can improve productivity when both sides need to meet demanding requirements.
Typical advantages include:
- Simultaneous processing of two faces
- Improved parallelism
- Controlled thickness
- High batch consistency
Common applications include:
- Precision washers
- Thin plates
- Ceramic components
- Semiconductor components
- Seal elements
- Spacers
For production parts with two critical parallel surfaces, double-sided lapping can be more efficient than processing each face independently.
Metal Lapping Service
A metal lapping service may be used after CNC machining, heat treatment, or grinding to finish critical metal surfaces.
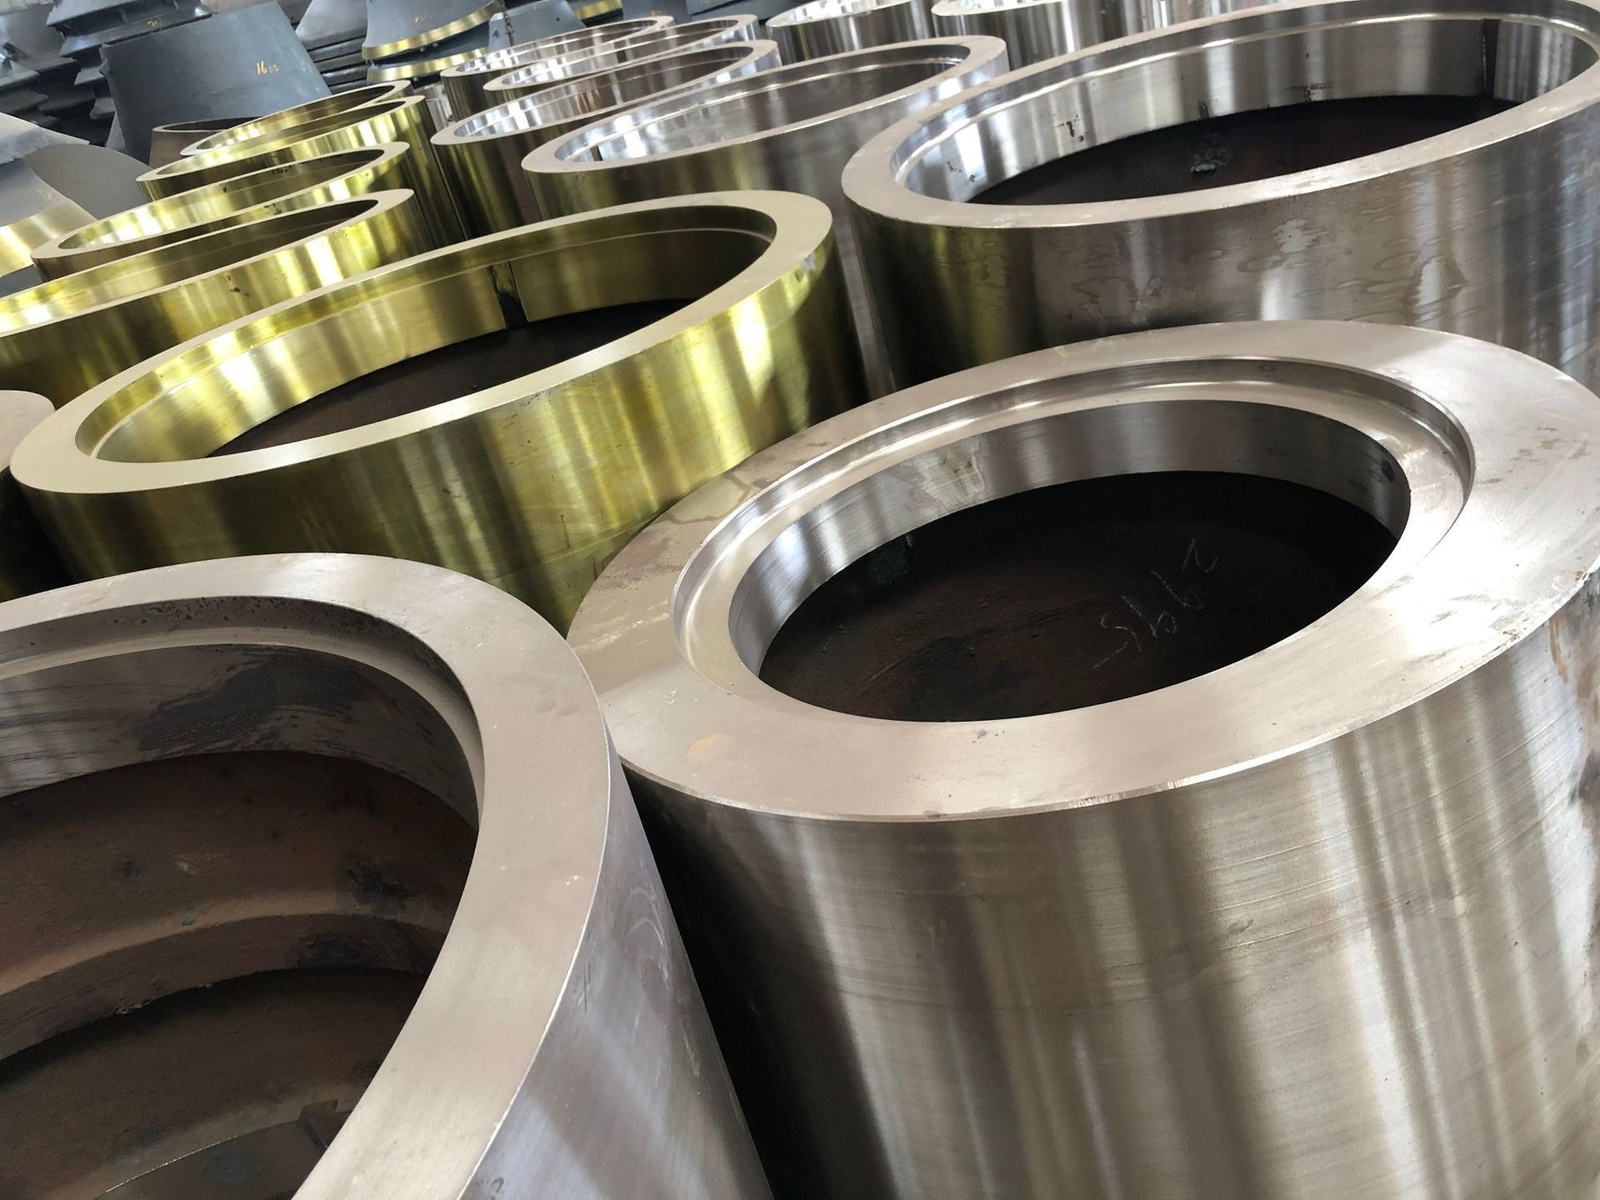
Common metallic materials include:
- Stainless steel
- Carbon steel
- Alloy steel
- Tool steel
- Aluminum
- Copper
- Brass
- Carbide
- Nickel alloys
- Titanium
The process must be adjusted for the material.
Abrasive selection, lap plate material, pressure, slurry chemistry, and process time can all change depending on hardness and surface behavior.
Lapping Stainless Steel
Stainless steel components are commonly lapped when they require:
- Precision sealing surfaces
- Fine flatness
- Low surface roughness
- Controlled thickness
Applications include:
- Valve components
- Medical equipment
- Vacuum hardware
- Semiconductor equipment
- Fluid-control parts
Because stainless steels vary significantly in hardness and machining behavior, the correct abrasive and lapping parameters depend on the specific grade.
Lapping Hardened Steel
Lapping is particularly useful after heat treatment.
A typical manufacturing sequence may be:
CNC machining → Heat treatment → Surface grinding → Precision lapping
Heat treatment can introduce small amounts of distortion.
Grinding restores the majority of the geometry.
Lapping can then refine the final surface where extremely tight flatness or finish is required.
Typical hardened components include:
- Valve plates
- Gauge components
- Tooling
- Wear plates
- Precision machine parts
Lapping Aluminum
Aluminum can also be lapped, but the process requires appropriate abrasive and plate selection.
Because aluminum is relatively soft compared with hardened steel or ceramics, inappropriate processing can create:
- Scratches
- Embedded abrasive
- Surface smearing
- Edge damage
The lapping process should therefore be selected according to both alloy and required final surface.
Lapping Ceramics and Hard Materials
Precision lapping is also widely used on hard, brittle materials.
Examples include:
- Alumina
- Zirconia
- Silicon carbide
- Sapphire
- Technical ceramics
Diamond abrasives are commonly used for very hard materials.
Applications include:
- Semiconductor equipment
- Optical components
- Electronic components
- Wear components
- Precision ceramic parts
The objective may include a combination of:
- Flatness
- Thickness
- Surface finish
- Edge quality
Lapping and Polishing: What Is the Difference?
The terms lapping and polishing are often used together, but they do not describe exactly the same objective.
Lapping
Lapping primarily focuses on:
- Geometry correction
- Flatness
- Parallelism
- Thickness
- Controlled material removal
- Surface refinement
Polishing
Polishing generally focuses more strongly on:
- Surface finish
- Reflectivity
- Cosmetic appearance
- Removal of very fine surface defects
A component may therefore be:
Ground → Lapped → Polished
depending on the final requirement.
The exact boundary between fine lapping and polishing can vary with the material and manufacturing process.
Precision Lapping vs. Surface Grinding
Surface grinding and lapping are both precision finishing processes, but they serve different stages of manufacturing.
| Feature | Surface Grinding | Precision Lapping |
|---|---|---|
| Material removal | Moderate | Very low |
| Abrasive | Bonded grinding wheel | Loose or controlled abrasive system |
| Flatness | Very good | Extremely high potential |
| Surface finish | Fine | Very fine |
| Production stage | Intermediate or final | Final finishing |
| Corrects large stock | Better | Poor |
| Precision thickness control | Good | Excellent for small final corrections |
Surface grinding is usually more efficient for bringing a component close to final thickness.
Lapping is then used when the remaining requirements exceed what grinding can reliably or economically provide.
For many precision components, the two processes are complementary.
Lapping vs. Milling
CNC milling is used to generate the basic component geometry.
It can create:
- Pockets
- Holes
- Slots
- Contours
- Flat faces
- Threads
- Complex 3D features
Modern CNC machining can produce excellent flat surfaces.
However, milling is not normally the first choice when a surface requires extremely tight flatness combined with a very fine finish.
A common process chain may therefore be:
CNC Milling → Surface Grinding → Lapping
Not every part requires all three stages.
The correct sequence depends entirely on the drawing requirements.
Lapping vs. Polishing
If the primary requirement is appearance or very low roughness, polishing may be sufficient.
If the primary requirement is dimensional surface geometry, lapping is generally more relevant.
For example:
A decorative stainless-steel panel may need polishing.
A mechanical seal face may need lapping.
An optical component may require both.
This distinction prevents an important engineering mistake:
A shiny surface is not necessarily a precision-flat surface.
Lapping vs. Honing
Lapping and honing are both abrasive finishing processes but are normally used for different geometries.
Lapping
Commonly used for:
- Flat surfaces
- Mating faces
- Precision thickness
- Surface flatness
Honing
Commonly used for:
- Internal cylindrical bores
- Bore roundness
- Cylindricity
- Bore surface texture
For example:
A hydraulic valve component may require:
- Honing inside a precision bore
- Lapping on a sealing face
Both processes may therefore appear on the same component.
How Much Material Does Lapping Remove?
Lapping is a finishing process.
It should normally remove only a small amount of material.
The ideal allowance depends on:
- Material
- Part size
- Initial flatness
- Previous machining process
- Surface roughness
- Heat-treatment distortion
- Final flatness
- Final thickness
- Required finish
There is no universal lapping allowance suitable for every component.
This is important during manufacturing planning.
If too little stock is left, lapping may not completely remove the previous machining pattern or geometric error.
If excessive stock is left, cycle time and cost increase significantly.
The best strategy is to control the preceding machining or grinding process so that lapping only performs the final precision correction.
Why Incoming Part Quality Matters
Lapping cannot economically rescue every badly machined component.
Suppose a part requires extremely tight final flatness but arrives at the lapping operation with:
- Heavy milling marks
- Significant bow
- Excessive taper
- Large thickness variation
The lapping cycle may become unnecessarily long.
It may also become difficult to maintain consistent dimensional control.
Good manufacturing process planning therefore considers lapping from the beginning.
For a precision custom part, this may mean controlling:
- Rough machining
- Stress relief
- Heat treatment
- Finish machining
- Grinding
- Lapping allowance
- Final inspection
The final result depends on the entire manufacturing sequence, not simply the last machine used.
How Precise Can Lapping Be?
This question is common, but quoting one universal number can be misleading.
The achievable result depends on:
- Component size
- Contact area
- Material
- Thickness
- Initial geometry
- Lap plate condition
- Abrasive size
- Machine configuration
- Temperature stability
- Inspection method
High-precision lapping systems are capable of controlling flatness at micron and, in specialized applications, sub-micron scales.
But a small ceramic component and a large steel plate should not be expected to achieve the same result under the same conditions.
Engineering drawings should define the actual functional requirement rather than simply asking for “the tightest possible flatness.”
How Is Lapped Flatness Measured?
High-precision flatness requires suitable inspection equipment.
Possible inspection methods include:
- Optical flats
- Monochromatic light
- Interferometry
- CMM
- Precision indicators
- Surface profilometry
- Specialized flatness measurement systems
The correct method depends on:
- Component size
- Flatness tolerance
- Surface reflectivity
- Material
- Application
For very tight flatness specifications, environmental stability can also become important.
Temperature variation affects both the workpiece and the measuring system.
What Does “Light Bands” Mean in Lapping Inspection?
For very flat reflective surfaces, an optical flat and monochromatic light can be used to evaluate flatness.
When the optical flat is placed over the component, interference fringes become visible.
These are commonly described as light bands.
The shape and spacing of these bands indicate how the surface deviates from the reference plane.
Straight and evenly spaced bands generally indicate a more uniform flat surface.
Curved bands indicate surface form deviation.
This measurement method is common where flatness requirements are substantially tighter than ordinary dimensional inspection.
Surface Finish After Lapping
Lapping can produce extremely smooth surfaces, but surface finish depends on many factors.
These include:
- Abrasive type
- Abrasive particle size
- Plate material
- Applied pressure
- Workpiece material
- Lapping time
- Slurry condition
- Incoming surface finish
A finer abrasive does not automatically guarantee a better result.
The entire lapping system must remain stable.
Abrasive contamination, plate condition, incorrect pressure, or poor cleaning can all cause scratches or inconsistent finish.
Edge Condition and Lapping
Edges require special attention during high-precision lapping.
Depending on the process and part geometry, excessive material removal near an edge can cause:
- Edge rounding
- Edge roll-off
- Loss of flatness near the perimeter
- Dimensional change
This matters particularly for:
- Sealing faces
- Optical parts
- Thin plates
- Gauge components
- Precision reference surfaces
If edge condition is functionally critical, it should be stated on the engineering drawing.
Common Precision Lapping Problems
Even a fine finishing process can produce poor parts if it is not controlled correctly.
Poor Flatness
Potential causes include:
- Lap plate not properly conditioned
- Uneven part distribution
- Incorrect pressure
- Poor motion pattern
- Excessive plate wear
Because the part tends to follow the geometry of the lapping plate, plate condition is fundamental to flatness control.
Scratches
Possible causes include:
- Oversized abrasive particles
- Contaminated slurry
- Foreign material
- Dirty workpieces
- Damaged lap plate
- Improper cleaning
This is particularly important when moving from coarse to fine lapping stages.
Excessive Edge Rounding
Possible causes include:
- Excessive processing time
- Incorrect pressure distribution
- Poor support
- Improper polishing conditions
Slow Material Removal
Potential causes include:
- Incorrect abrasive
- Glazed or poorly conditioned plate
- Inadequate pressure
- Incorrect slurry concentration
- Material/abrasive mismatch
Maintaining predictable plate texture and geometry is important for consistent material-removal rates.
Uneven Thickness
Potential causes include:
- Incoming thickness variation
- Uneven loading
- Incorrect plate condition
- Poor part distribution
- Incorrect process settings
Typical Applications of Precision Lapping
Precision lapping is used where the relationship between two surfaces directly affects component performance.
Mechanical Seals
Seal faces must contact uniformly.
Excessive surface deviation can create leakage paths.
Lapping helps produce controlled flat sealing surfaces.
Valve Components
Valve plates and sealing elements may require accurate surfaces to control:
- Leakage
- Contact
- Pressure
- Movement
Lapping is often applied after machining or grinding.
Pump Components
Pump components can contain precision mating surfaces where flatness and surface finish affect sealing efficiency.
Semiconductor Equipment
Semiconductor manufacturing equipment may require components with:
- Tight flatness
- Precise thickness
- High surface quality
- Controlled contamination
Materials can include:
- Stainless steel
- Aluminum
- Ceramics
- Specialty materials
Optical Components
Optical systems frequently require extremely controlled surface geometry.
Lapping may be used before final polishing to establish:
- Flatness
- Thickness
- Surface form
Aerospace Components
Lapping may be applied to precision:
- Valve components
- Hydraulic parts
- Sealing faces
- Instrument components
The process is selected only where the drawing and functional requirements justify the additional finishing operation.
Medical Components
Medical equipment can contain precision mating surfaces, valve components, and instrument parts requiring controlled geometry and finish.
Material cleanliness and post-lapping cleaning are particularly important in these applications.
When Should You Specify Precision Lapping?
Not every machined surface needs lapping.
In fact, specifying lapping unnecessarily increases cost.
Consider precision lapping services when one or more of the following conditions apply.
Flatness Is Functionally Critical
Examples include:
- Mechanical sealing
- Vacuum sealing
- Optical alignment
- Precision reference surfaces
Very Tight Parallelism Is Required
Especially on thin precision plates or spacers.
The Surface Must Meet Another Surface Uniformly
For example:
- Valve plates
- Seal faces
- Gauge surfaces
Grinding Cannot Consistently Meet the Final Requirement
Lapping can be used as a final correction step.
Very Fine Surface Finish Is Required Together With Flatness
This combination is one of the most common reasons for selecting lapping.
The Part Requires Final Micron-Level Thickness Adjustment
Small final dimensional corrections can be made without returning the part to heavy machining.
When Is Lapping Unnecessary?
Lapping should not become a default finishing requirement.
It may be unnecessary when:
- Standard CNC milling meets the functional requirement
- Surface grinding already meets flatness and finish requirements
- The component is non-critical
- The requirement is cosmetic rather than geometric
- The drawing contains unnecessarily tight tolerances
For example, specifying extreme flatness on a mounting bracket with no precision mating function may increase cost without improving the product.
Good engineering defines the necessary tolerance, not simply the smallest possible tolerance.
How Should Lapping Be Specified on an Engineering Drawing?
Simply writing:
LAP SURFACE
is usually incomplete.
The drawing should communicate what the surface actually needs to achieve.
Flatness
Example:
Flatness 0.003 mm
Use the tolerance required by the function.
Parallelism
If the lapped face must remain parallel to another datum surface, specify parallelism separately.
Thickness
If lapping establishes final part thickness, define the appropriate thickness tolerance.
Surface Roughness
Example:
Ra ≤ 0.1 μm
Only specify a value appropriate to the application.
Surface Area
Clearly identify which face or faces require lapping.
Do not require every surface to receive a precision finishing operation unless necessary.
Edge Requirements
If edges must remain sharp or edge roll-off is limited, define the requirement.
Cosmetic Requirements
If scratches or visual marks are unacceptable, state this independently from roughness and flatness.
Cosmetic quality and dimensional surface quality are not always the same thing.
Precision Lapping and Small-Batch Custom Parts
Lapping is sometimes associated with highly specialized mass-production processes, but it can also be valuable for prototypes and small-batch precision components.
The important question is not production quantity.
It is whether the part function requires the process.
For a prototype valve, optical fixture, semiconductor component, precision seal, or medical assembly, producing only 5, 20, or 100 parts does not make the flatness requirement less important.
In these projects, lapping is often integrated into a broader manufacturing route such as:
CNC machining → Heat treatment → Grinding → Lapping → Inspection
This is particularly relevant to custom parts because manufacturing engineers must coordinate all of these operations around the same drawing requirements.
At 6CNC, this is where the focus on small-batch custom precision machining becomes important: the objective is not to apply the greatest possible number of finishing processes, but to determine which operations are actually necessary to move a precision component from prototype into repeatable small-batch production.
Precision Lapping vs. Over-Tolerancing
One of the easiest ways to make a lapped component unnecessarily expensive is to specify requirements beyond what the application needs.
For example, a drawing might request:
- Extremely tight flatness
- Extremely low Ra
- Very tight thickness
- Tight parallelism
all on the same component.
Every individual requirement may be technically possible.
But the combination can significantly increase:
- Processing time
- Inspection time
- Scrap risk
- Cost
Before specifying high-precision lapping, ask:
What does this surface actually need to do?
Does it need to:
- Seal?
- Locate?
- Slide?
- Reflect?
- Control spacing?
- Maintain vacuum?
- Transfer force uniformly?
The functional answer should determine the tolerance.
What Information Should You Send for a Precision Lapping Quote?
For an accurate metal lapping service or precision lapping quotation, provide:
- 2D engineering drawing
- 3D CAD model where available
- Material
- Heat-treatment condition
- Part dimensions
- Surfaces requiring lapping
- Flatness requirement
- Parallelism requirement
- Final thickness
- Surface roughness
- Edge requirements
- Cosmetic requirements
- Quantity
- Inspection requirements
Also indicate the function of the surface when possible.
Knowing that a face is used for a mechanical seal, optical reference, or precision spacer can help manufacturing engineers understand which characteristics are genuinely critical.
Choosing Between Machining, Grinding, Lapping, and Polishing
The final manufacturing process should be determined by the required result.
| Requirement | Typical Process |
|---|---|
| Create overall geometry | CNC machining |
| Remove moderate stock from flat surface | Surface grinding |
| Improve precision flatness | Lapping |
| Control very precise thickness | Grinding / lapping |
| Produce very fine surface | Lapping / polishing |
| Improve cosmetic reflectivity | Polishing |
| Finish precision bore geometry | Honing |
These processes are not competitors in every situation.
They often work together.
A precision component might require:
5-axis machining → Heat treatment → Surface grinding → Lapping
while another component may need only:
CNC milling
Using fewer processes is generally preferable when they meet the functional requirement.
Precision manufacturing is not about applying the most advanced process.
It is about applying the correct process.
Precision Lapping Services for Custom Machined Parts
Precision lapping is a specialized finishing process for components where the last few microns matter.
Its value is not simply producing a surface that looks smooth.
The process can improve:
- Flatness
- Parallelism
- Thickness
- Surface finish
- Surface contact
- Functional sealing
For engineers sourcing custom parts, lapping should therefore be considered part of the complete manufacturing strategy rather than an isolated surface treatment.
Good results begin with correct CNC machining and grinding allowances, continue through controlled lapping, and end with inspection that verifies the actual drawing requirements.
6CNC supports custom precision parts from prototype through small-batch production, including projects where CNC machining must be combined with precision grinding, honing, lapping, and other secondary processes to achieve final functional requirements.
If your drawing contains critical flatness, parallelism, thickness, or surface-finish requirements, send the drawing and CAD files for manufacturing review before finalizing the production route.
Frequently Asked Questions
What is precision lapping?
Precision lapping is a fine abrasive finishing process that removes very small amounts of material to improve surface flatness, parallelism, thickness, and surface finish. It is commonly used after machining or grinding when the final surface requirement is more demanding than conventional machining can achieve economically.
What is flat lapping?
Flat lapping processes a planar surface against a controlled lapping plate using abrasive particles. It is commonly used for seal faces, valve plates, spacers, ceramics, optical components, and other parts requiring high flatness.
What is the difference between lapping and polishing?
Lapping generally focuses more on geometry, including flatness, parallelism, and thickness, while polishing focuses more heavily on final surface finish and appearance. Some high-precision components require both processes.
What is the difference between lapping and grinding?
Grinding removes material using a bonded abrasive wheel and generally provides a higher material-removal rate. Lapping removes much smaller amounts of material and is used when exceptional flatness or surface quality is required. Grinding is often performed before lapping.
Can metal parts be lapped?
Yes. Common lapped metals include stainless steel, carbon steel, alloy steel, tool steel, aluminum, copper alloys, titanium, and nickel alloys. Abrasive and processing conditions must be selected for the specific material.
Can hardened steel be lapped?
Yes. Hardened components are commonly ground first and then lapped where extremely accurate flatness or fine surface finish is required.
Does a low Ra value mean the surface is flat?
No. Surface roughness and flatness describe different characteristics. A surface can be extremely smooth but still have bow, waviness, or other form errors.
Can lapping improve parallelism?
Yes. Lapping, particularly double-sided lapping, can be used to improve parallelism between opposing surfaces while controlling final thickness.
How much material does lapping remove?
Lapping normally removes only a small finishing allowance. The amount depends on the material, incoming geometry, component size, and final requirements. It should not normally be used as a replacement for rough machining or heavy grinding.
What is high precision lapping used for?
High precision lapping is used for parts where very small deviations in flatness, parallelism, thickness, or surface finish affect component performance. Examples include mechanical seals, valves, optical components, semiconductor equipment, gauges, and precision machine components.
Is lapping suitable for prototypes and small batches?
Yes. Lapping can be used for prototypes and small-batch parts when the functional surface requirements justify the process. Production quantity does not determine whether lapping is technically necessary.
What information is needed for a precision lapping quote?
Provide the material, heat treatment, part dimensions, lapped surfaces, flatness requirement, parallelism, final thickness, surface roughness, quantity, edge requirements, and engineering drawings. Functional information about the critical surface can also help determine the correct process.


