
6CNC · PROTOTYPES · SMALL BATCHES
Custom CNC Machined Connectors
6CNC manufactures custom CNC machined connectors for applications where fit, alignment, sealing, conductivity, or mechanical strength cannot be left to standard off-the-shelf components.
Our CNC machining capabilities support prototypes, engineering validation builds, replacement components, and small-batch production from 1 to 600 parts.
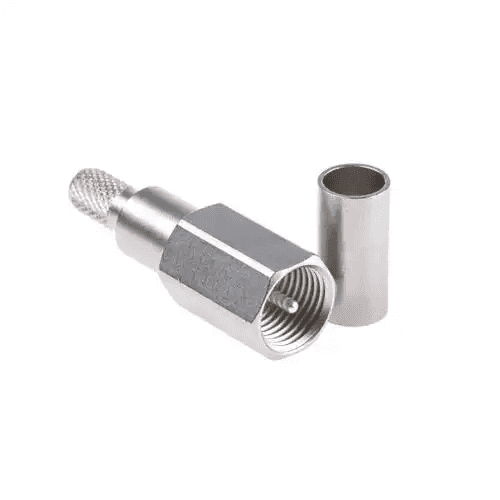
Connector Types We Manufacture
Explore the connector families below. We manufacture custom components from your drawings, CAD models and functional requirements.
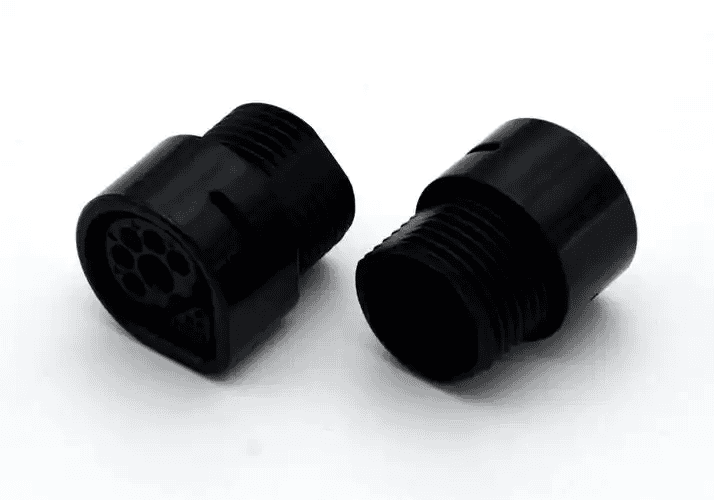
Electrical Connector Components
Shells, housings, receptacles, terminals and contact retainers for electrical interfaces.
Features and machining considerations
Precision machined electrical connectors are commonly used where molded or stamped components cannot provide the required mechanical strength, dimensional accuracy, shielding, or environmental resistance.
Typical components include:
- Connector shells
- Connector housings
- Receptacle bodies
- Plug bodies
- Cable backshells
- Threaded coupling rings
- Terminal components
- Contact retainers
- Shielding components
Materials such as aluminum, stainless steel, brass, and copper alloys can be selected according to conductivity, weight, corrosion resistance, strength, and finishing requirements.
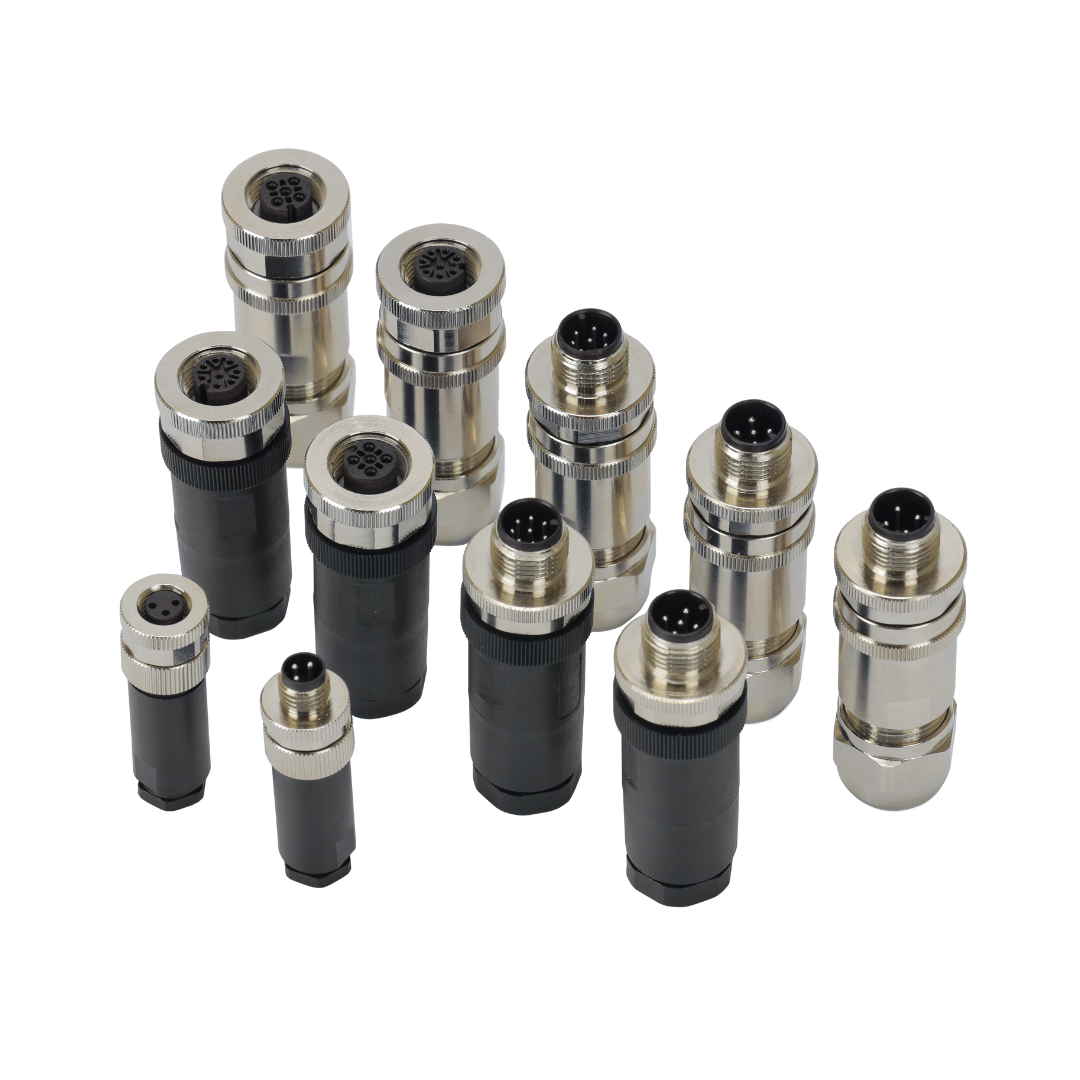
Circular Connector Components
Concentric shells, coupling rings and mating interfaces with threads, seals and anti-rotation features.
Features and machining considerations
Circular connectors often rely on accurate concentric geometry.
For example, a circular connector shell may contain an internal thread, external locating diameter, sealing groove, anti-rotation feature, and mating shoulder. Small dimensional errors between these features can cause poor engagement, misalignment, leakage, or premature wear.
CNC turning and mill-turn machining are commonly used to keep these features referenced from consistent datums.
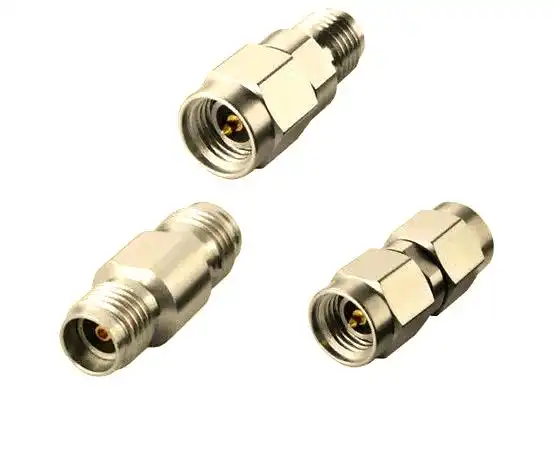
RF and Coaxial Connector Components
Compact threaded bodies with fine features, controlled concentricity and smooth mating surfaces.
Features and machining considerations
RF connector components often require very small geometry and controlled concentricity between internal and external features.
Typical requirements can include:
- Fine threads
- Thin walls
- Small precision bores
- Tight concentricity
- Smooth mating surfaces
- Controlled contact geometry
Brass, copper alloys, stainless steel, and aluminum are commonly used depending on the design.
Surface finishes such as nickel plating, gold plating, passivation, or anodizing may also be specified.
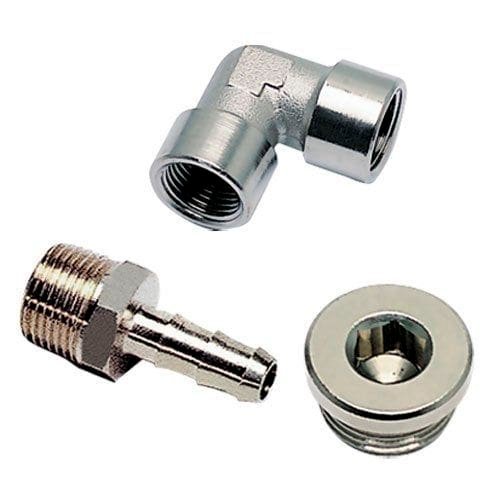
Hydraulic and Pneumatic Connectors
Pressure-sealing connectors with pipe threads, O-ring grooves, precision bores and wrench flats.
Features and machining considerations
Hydraulic and pneumatic connectors must maintain dimensional accuracy while also providing reliable pressure sealing.
Common machined features include:
- Tapered threads
- Straight threads
- O-ring grooves
- Sealing cones
- Precision bores
- Wrench flats
- Cross-drilled ports
- Shoulder surfaces
For these parts, thread quality and sealing geometry can be more important than the overall appearance of the component.
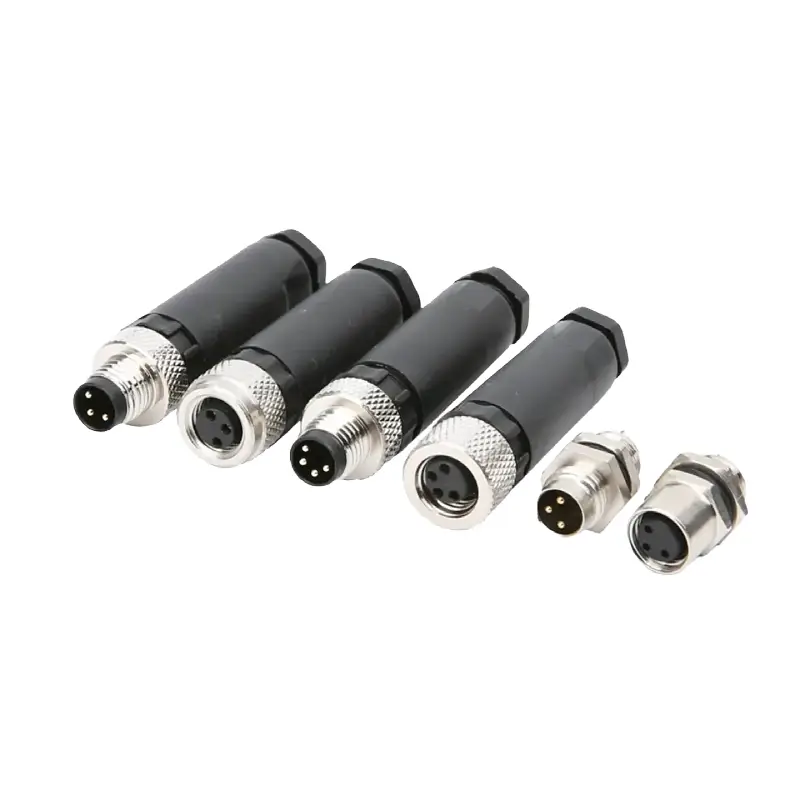
Sensor and Instrumentation Connectors
Compact sensor interfaces with M8, M12 or custom threads, cable routing and sealing shoulders.
Features and machining considerations
Sensor connectors can be extremely compact while incorporating multiple functional features.
For example, a stainless steel sensor connector may require:
- M8, M12, or custom threads
- A precision internal bore
- Cable routing
- A sealing shoulder
- Wrench flats
- Laser-marking areas
These parts are commonly used in automation equipment, robotics, industrial measurement systems, medical equipment, and process-control systems.
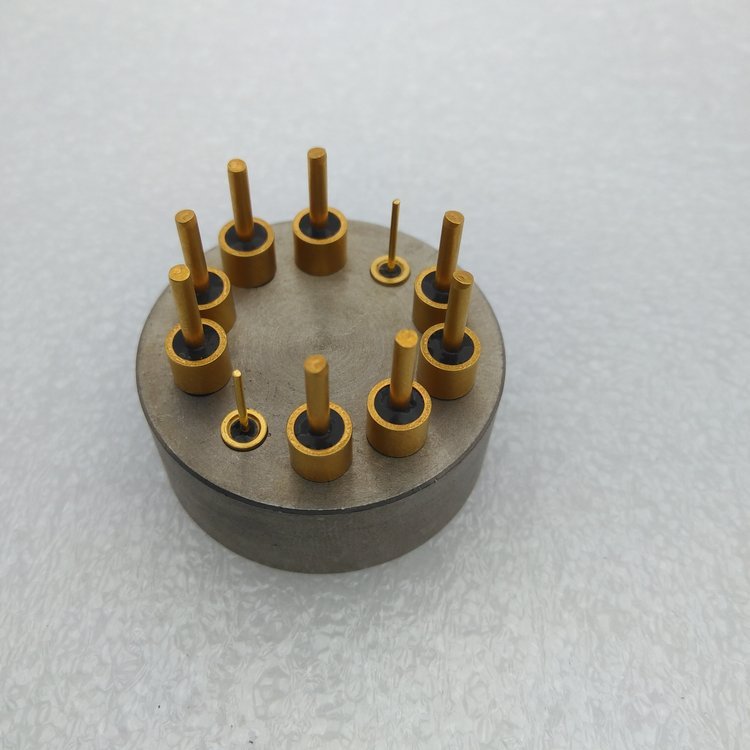
Vacuum and Fluid Connectors
Vacuum and fluid interfaces planned around sealing surfaces, port alignment and cleanliness.
Features and machining considerations
Fluid and vacuum systems depend heavily on sealing-surface quality.
We machine components such as:
- Vacuum fittings
- Fluid adapters
- Tube connectors
- Manifold connectors
- Hose adapters
- Custom threaded fittings
- Instrumentation fittings
The machining process can be planned around sealing surfaces, port alignment, thread engagement, and cleanliness requirements.
Choose the Right Machining Process
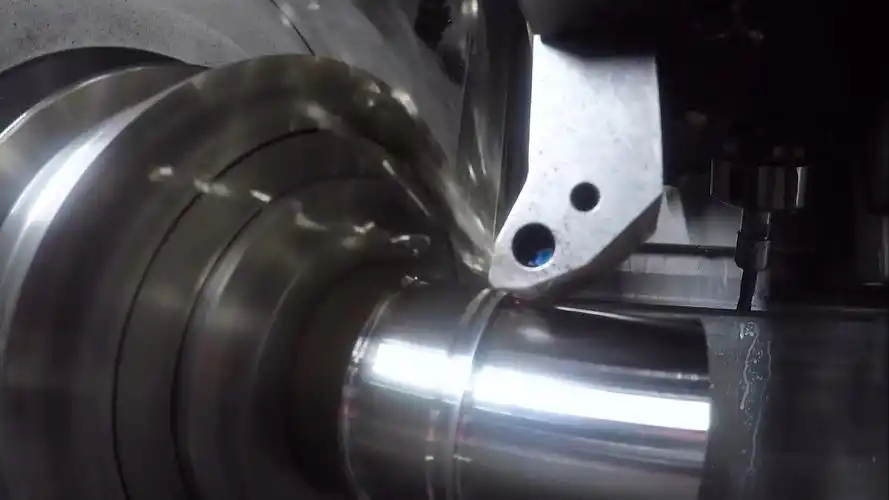
CNC Turning
For rotational shells, sleeves and couplings with concentric bores, threads and sealing diameters.
Features and machining considerations
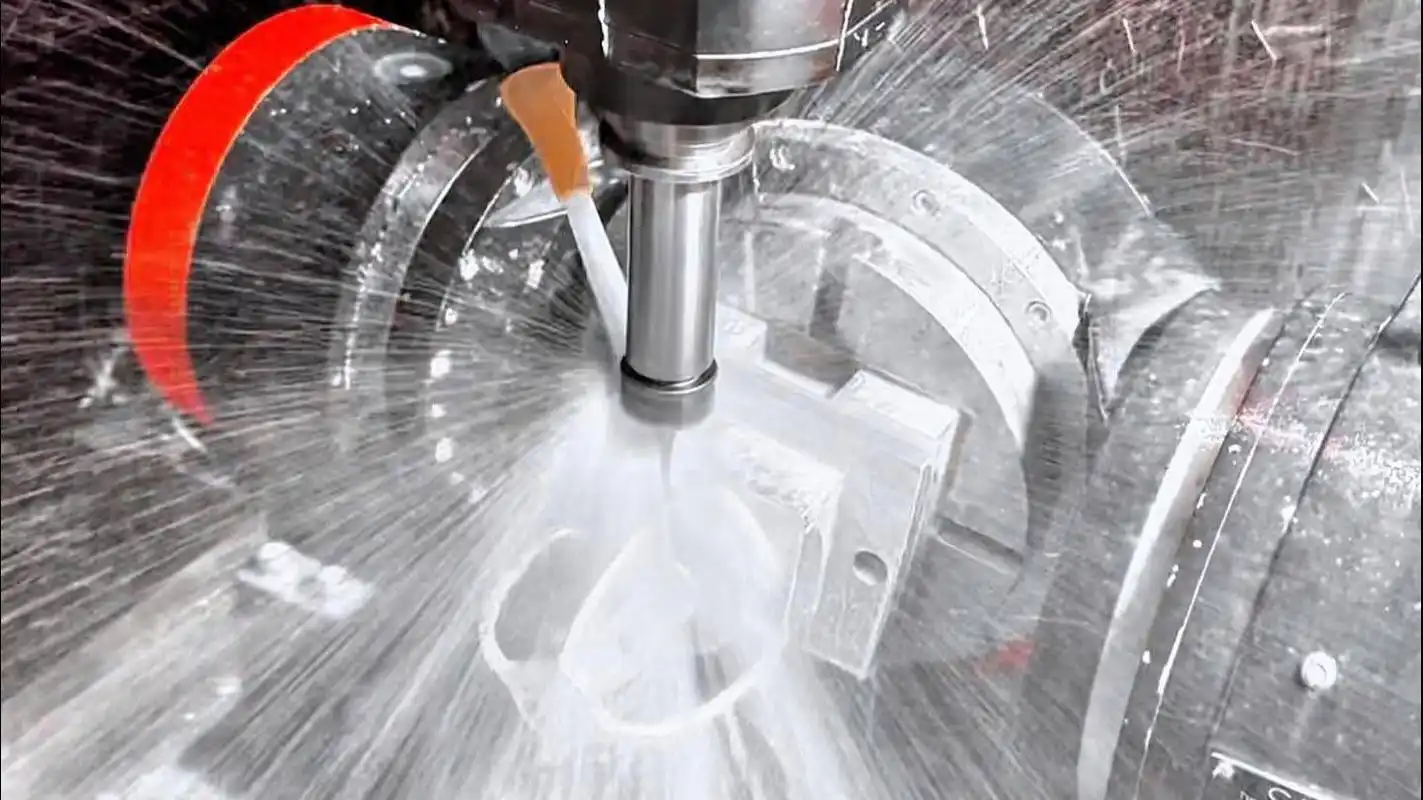
CNC turning is widely used for circular and rotational connector components such as:
- Connector shells
- Threaded sleeves
- Couplings
- Bushings
- Receptacles
- Pins
- Ferrules
- Adapter bodies
- Hydraulic connectors
- Sensor fittings
For connector parts with concentric bores, threads, grooves, and sealing diameters, turning provides efficient control of roundness and coaxial relationships.
CNC Milling
For flats, mounting faces, slots, side holes and other non-rotational connector features.
Features and machining considerations
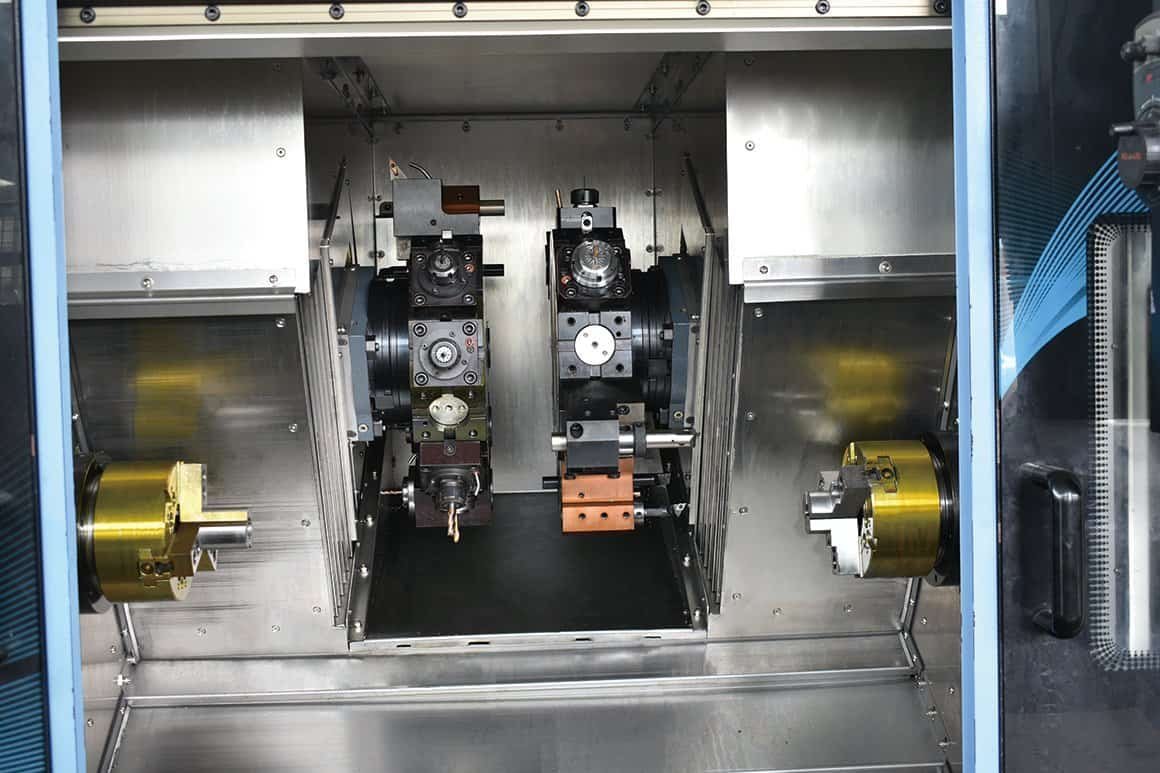
CNC milling is suitable for connector components requiring non-rotational features such as:
- Flats
- Mounting faces
- Keyways
- Slots
- Bolt patterns
- Side holes
- Cable-entry features
- Anti-rotation geometry
- Locating features
Milling can also be combined with turning for connectors that contain both cylindrical and prismatic geometry.
Mill-Turn Machining
Combines turned and milled features in fewer setups to maintain their positional relationship.
Features and machining considerations
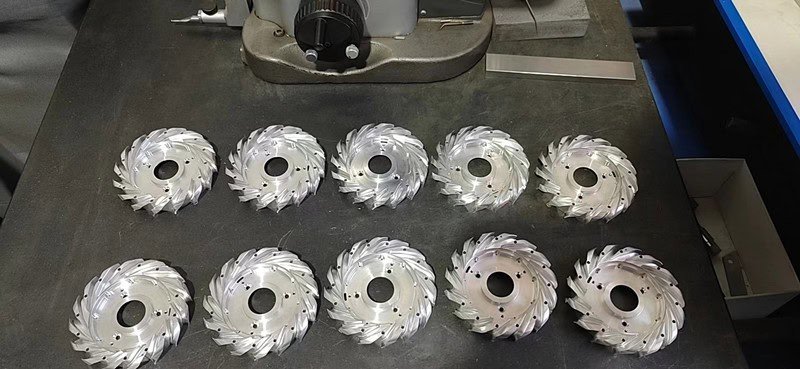
Mill-turn machining is particularly useful for complex connector bodies.
A part may require an external thread, precision bore, cross-hole, wrench flat, sealing groove, and mounting feature. Producing these features in fewer setups can improve positional consistency and reduce handling between operations.
5-Axis CNC Machining
For angled ports, compound geometry and features that are difficult to access from one direction.
Features and machining considerations
For specialized aerospace, optical, robotic, medical, or instrumentation connectors, 5-axis machining can be used for complex geometry, angled ports, compound surfaces, and difficult-to-access features.
Materials and Surface Finishes
Material selection affects machining behavior, strength, conductivity, corrosion resistance, weight, sealing performance, and surface finishing.
6CNC machines a wide range of metals and engineering plastics for custom connector applications.
| Material | Common Connector Applications | Key Advantages |
|---|---|---|
| Aluminum 6061 | Electronic housings, aerospace connectors, lightweight adapters | Lightweight, machinable, corrosion resistant |
| Aluminum 7075 | Aerospace and structural connector components | High strength-to-weight ratio |
| Stainless Steel 304 | Industrial and general-purpose connectors | Corrosion resistance and durability |
| Stainless Steel 316/316L | Marine, medical, fluid, and chemical connectors | Excellent corrosion resistance |
| Stainless Steel 17-4PH | High-strength connector components | High strength and good corrosion resistance |
| Brass | Electrical connectors, terminals, fittings | Excellent machinability and good conductivity |
| Copper | Electrical and thermal connector components | High electrical and thermal conductivity |
| Titanium Grade 5 | Aerospace, medical, and high-performance connectors | High strength, low weight, corrosion resistance |
| PEEK | Electrical isolation and high-temperature connectors | Heat resistance and dimensional stability |
| POM / Delrin | Insulators, sleeves, connector inserts | Low friction and good dimensional stability |
| PTFE | Chemical and fluid connector components | Chemical resistance and electrical insulation |
Finishing options and coating allowance
Surface treatment can improve connector corrosion resistance, wear resistance, conductivity, appearance, or environmental protection.
Available finishing options include:
- As machined
- Bead blasting
- Anodizing
- Hard anodizing
- Passivation
- Electroless nickel plating
- Nickel plating
- Zinc plating
- Black oxide
- Powder coating
- Polishing
- Electropolishing
- Gold plating through qualified finishing partners
- Custom finishing according to drawing requirements
Anodized Aluminum Connectors
Anodizing is commonly used on aluminum connector housings and shells.
It can improve corrosion resistance and wear resistance while also providing a controlled appearance.
However, anodizing adds coating thickness. Threads, precision mating diameters, and electrical contact areas may therefore require masking or dimensional compensation.
Passivated Stainless Steel Connectors
Passivation is widely used on stainless steel connector components for medical, marine, food-processing, and industrial equipment.
It helps improve corrosion performance without significantly changing component dimensions.
Plated Brass and Copper Connectors
Brass and copper components may be plated where improved corrosion resistance, conductivity behavior, solderability, wear resistance, or appearance is required.
Plating thickness should be considered when defining final mating dimensions.
Precision, Tolerances and Design
Actual tolerances depend on material, feature size, geometry, wall thickness, process, and inspection requirements.
For precision connector components, commonly controlled characteristics may include:
| Feature | Typical Requirement |
|---|---|
| General CNC dimensions | ±0.05 mm |
| Precision dimensions | ±0.01 mm or tighter where appropriate |
| Precision bores | Based on fit requirement |
| Thread features | According to specified thread class |
| Concentricity / runout | Controlled according to functional requirement |
| Hole position | Defined according to drawing and datum scheme |
| Surface roughness | Selected according to sealing, sliding, or cosmetic function |
Functional features
Mating Diameters
Male and female connector components must fit correctly without excessive looseness, interference, or misalignment.
Important dimensions can include:
- Male outside diameter
- Female bore diameter
- Locating shoulders
- Guide diameters
- Insert diameters
These features may require tighter tolerances than the non-functional external surfaces of the same component.
Threaded Features
Threads are among the most common functional features in connector machining.
We can machine:
- Metric threads
- Unified threads
- Internal threads
- External threads
- Fine-pitch threads
- Pipe threads
- Custom thread forms
Thread requirements should specify the standard, pitch, class, and any required gauges or inspection methods.
Small connector components often contain thin walls around internal threads, so machining strategy and workholding must be considered carefully to avoid deformation.
Concentricity and Runout
Circular connector bodies commonly contain several coaxial features.
For example:
External mating diameter → internal bore → thread → sealing diameter
If these features are produced from unrelated setups, tolerance stack-up may affect final assembly.
Where practical, 6CNC machines related rotational features from the same setup or datum structure to maintain better alignment.
Sealing Surfaces
Hydraulic, pneumatic, fluid, and vacuum connectors may depend on:
- O-ring grooves
- Gasket faces
- Sealing cones
- Flat sealing faces
- Precision cylindrical seals
These surfaces may require tighter dimensional control and lower roughness than non-sealing areas.
Position and Alignment
Cross-holes, mounting holes, slots, keyways, and cable exits often need to maintain a defined angular or positional relationship with threads or other mating features.
These relationships should be defined with appropriate datums and GD&T where functionally necessary.
Design checklist
Avoid Unnecessarily Thin Walls
Thin sections can deform during clamping or machining, particularly around internal threads and deep bores.
Where possible, provide sufficient wall thickness around high-stress or threaded features.
Define Functional Datums
If a connector contains several mating features, the drawing should clearly define which surface or axis controls their relationship.
This helps machining and inspection use the same functional reference system.
Separate Cosmetic and Functional Requirements
A cosmetic external surface does not necessarily require the same tolerance or roughness as a sealing face.
Separating these requirements can reduce unnecessary machining cost.
Consider Coating Thickness
Anodizing and plating change finished dimensions.
Critical threads, bores, and mating surfaces should be reviewed before finishing so coating allowance or masking can be included in the manufacturing plan.
Specify Threads Completely
A thread note should clearly identify:
- Thread standard
- Nominal size
- Pitch
- Internal or external thread
- Thread class where required
- Depth
- Special inspection requirements
Incomplete thread specifications are a common source of manufacturing delays.
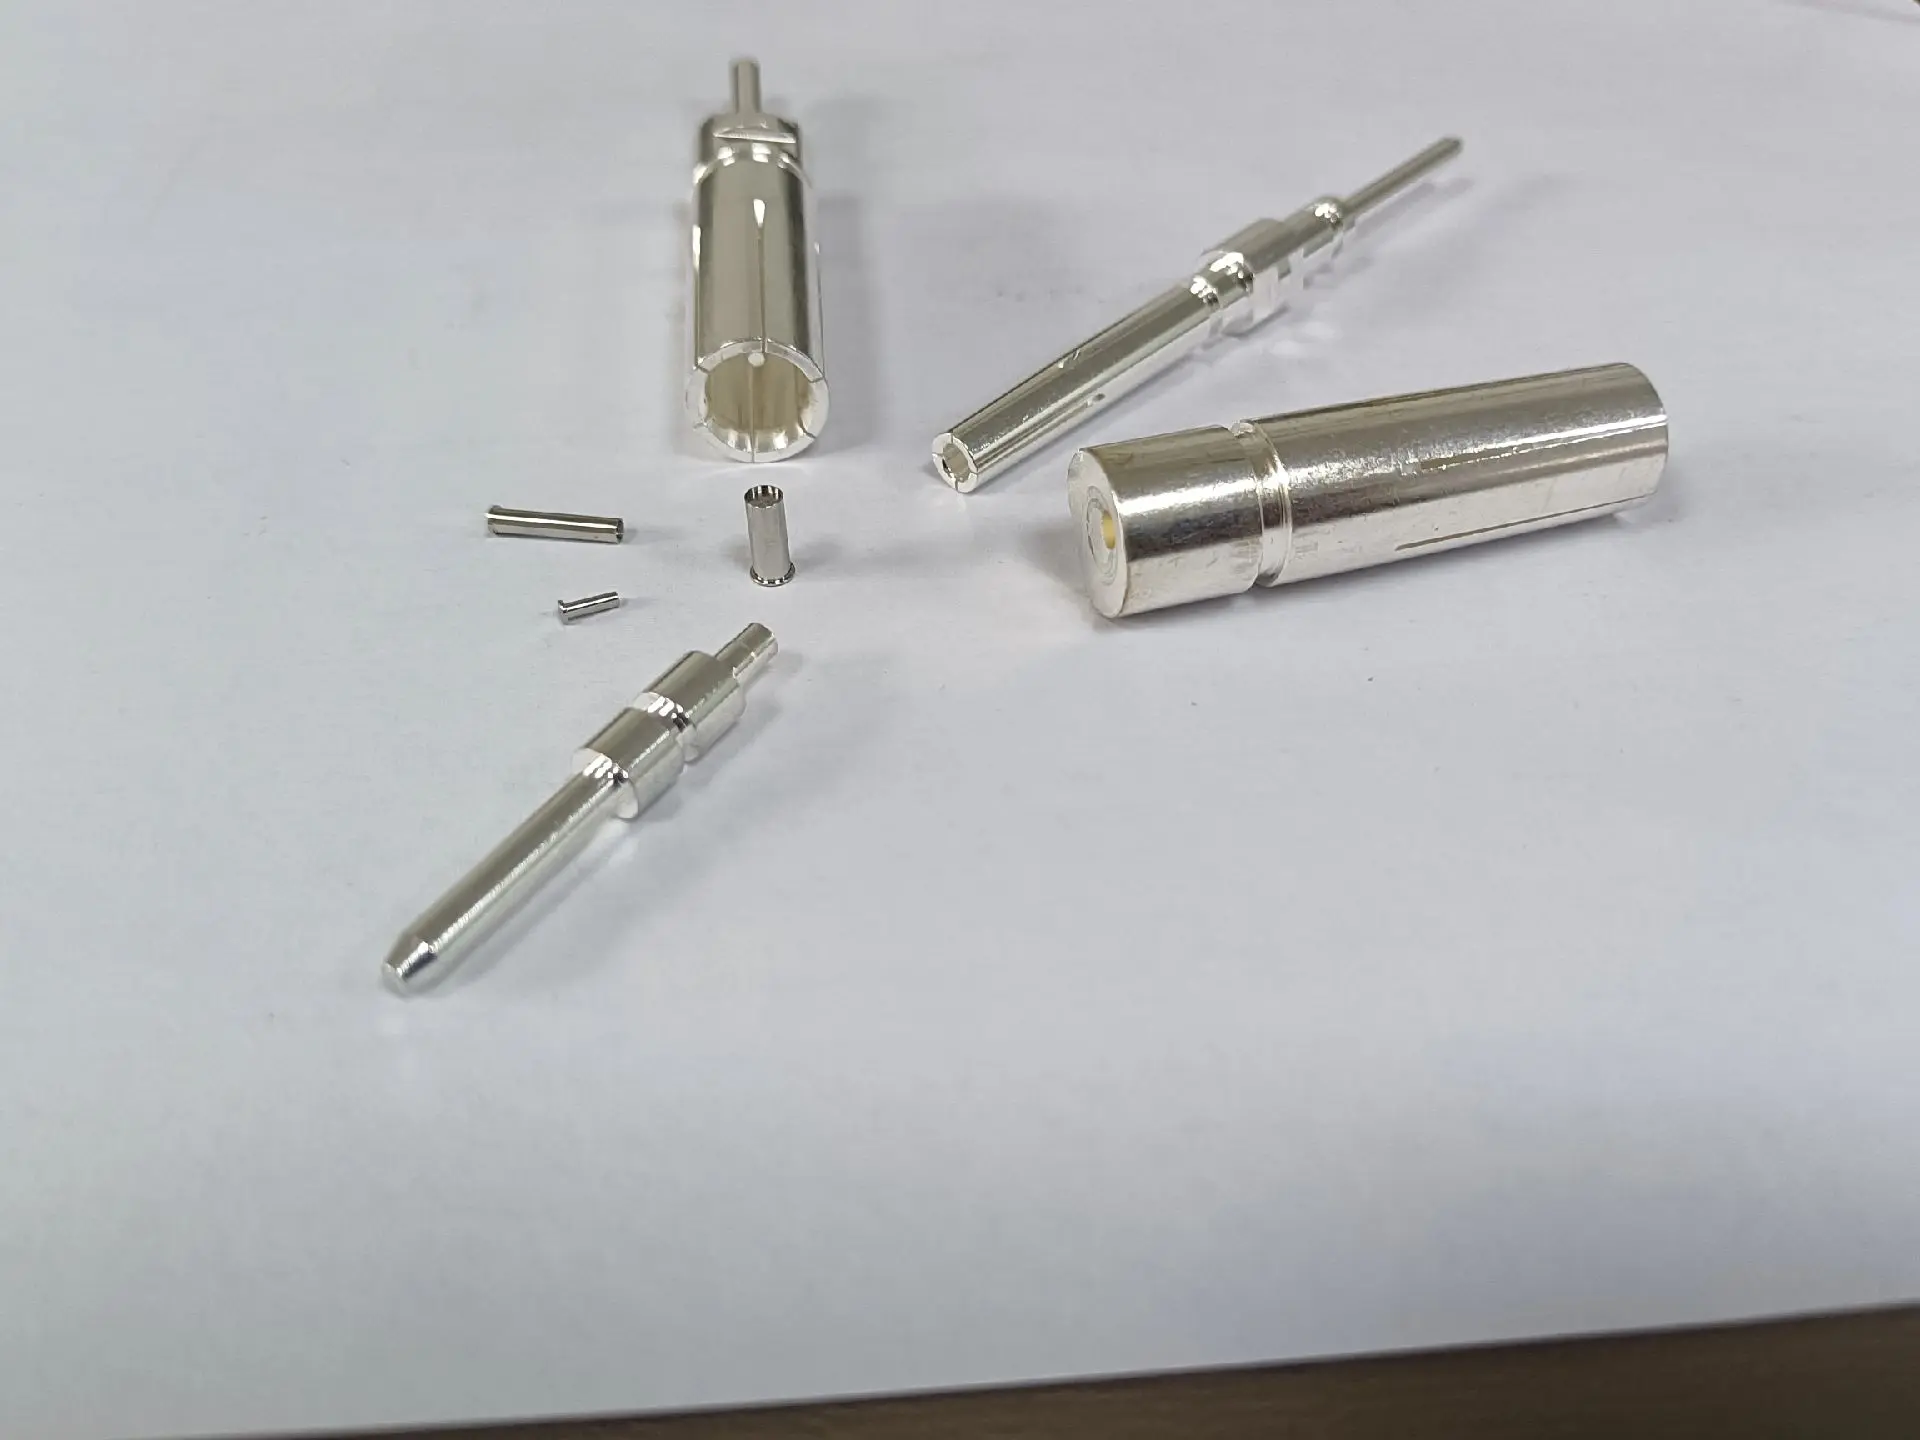
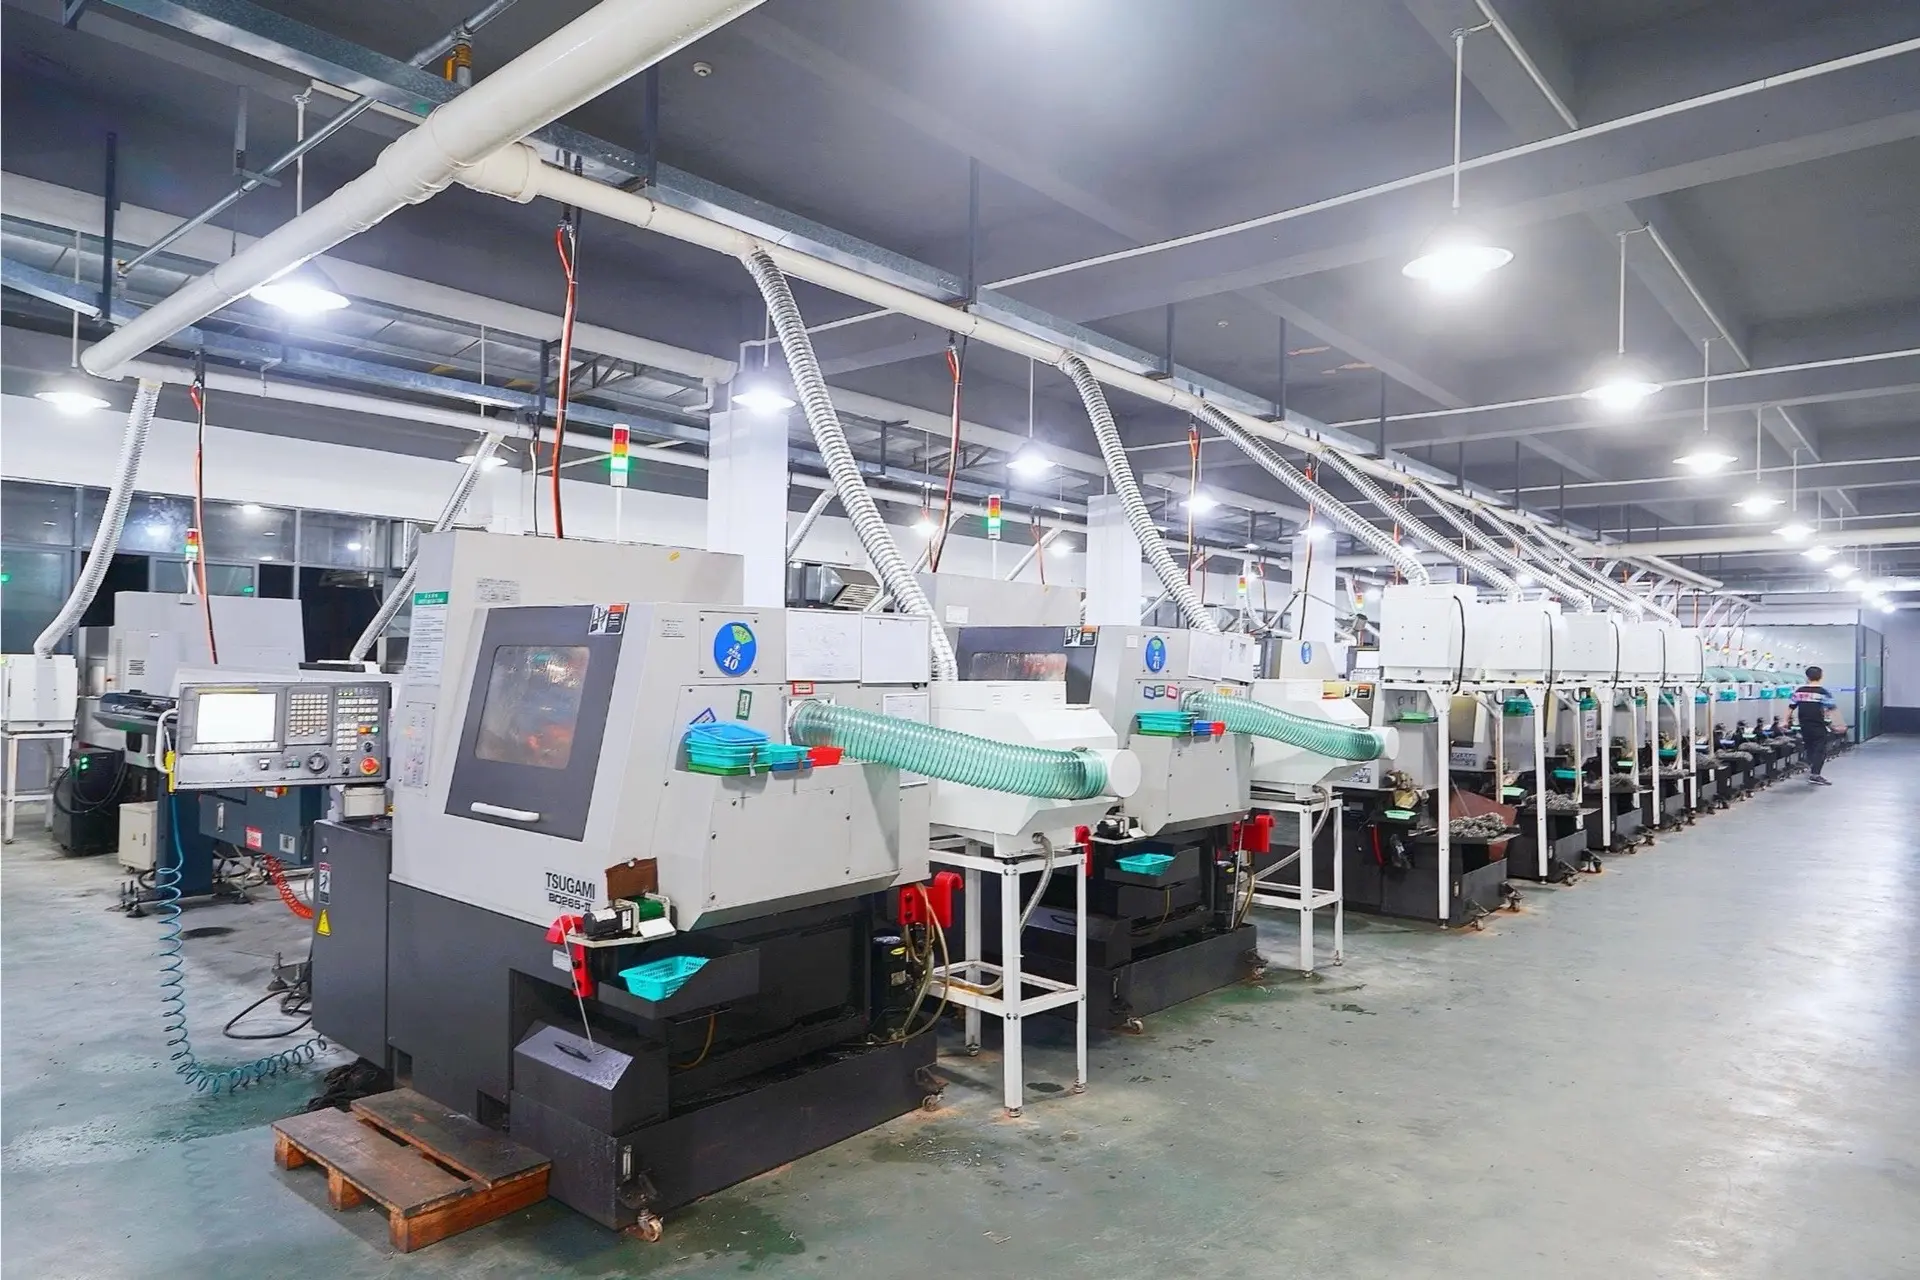
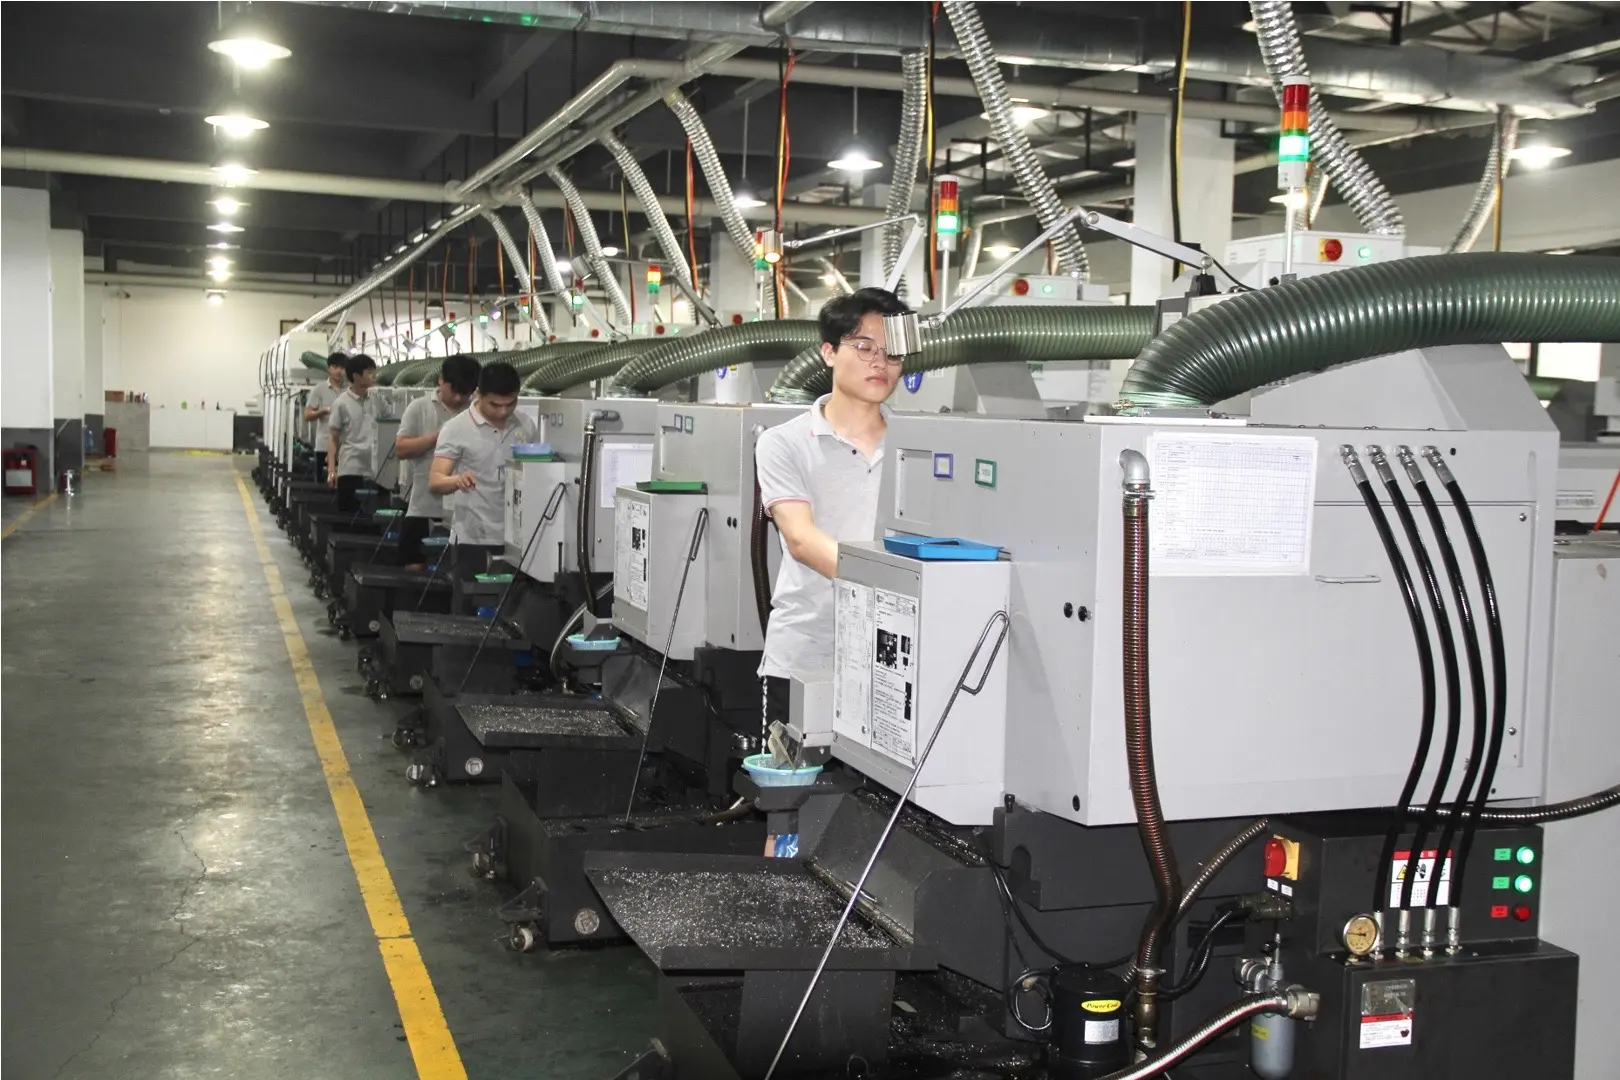
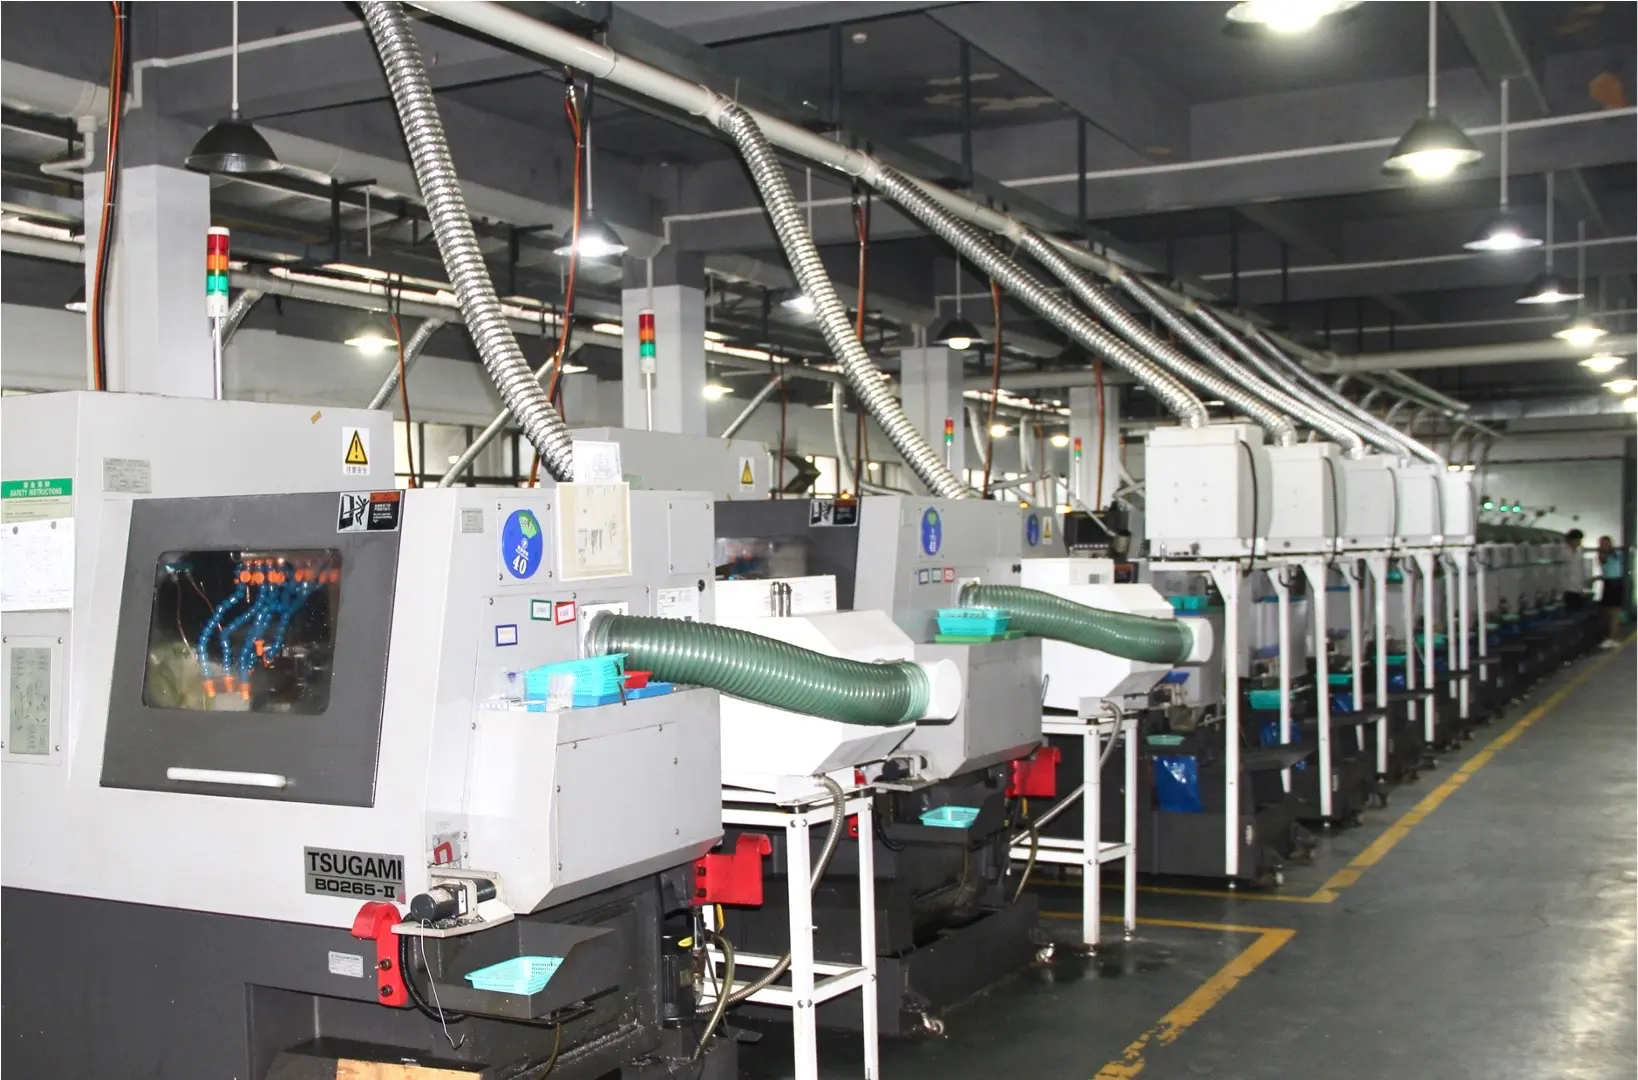
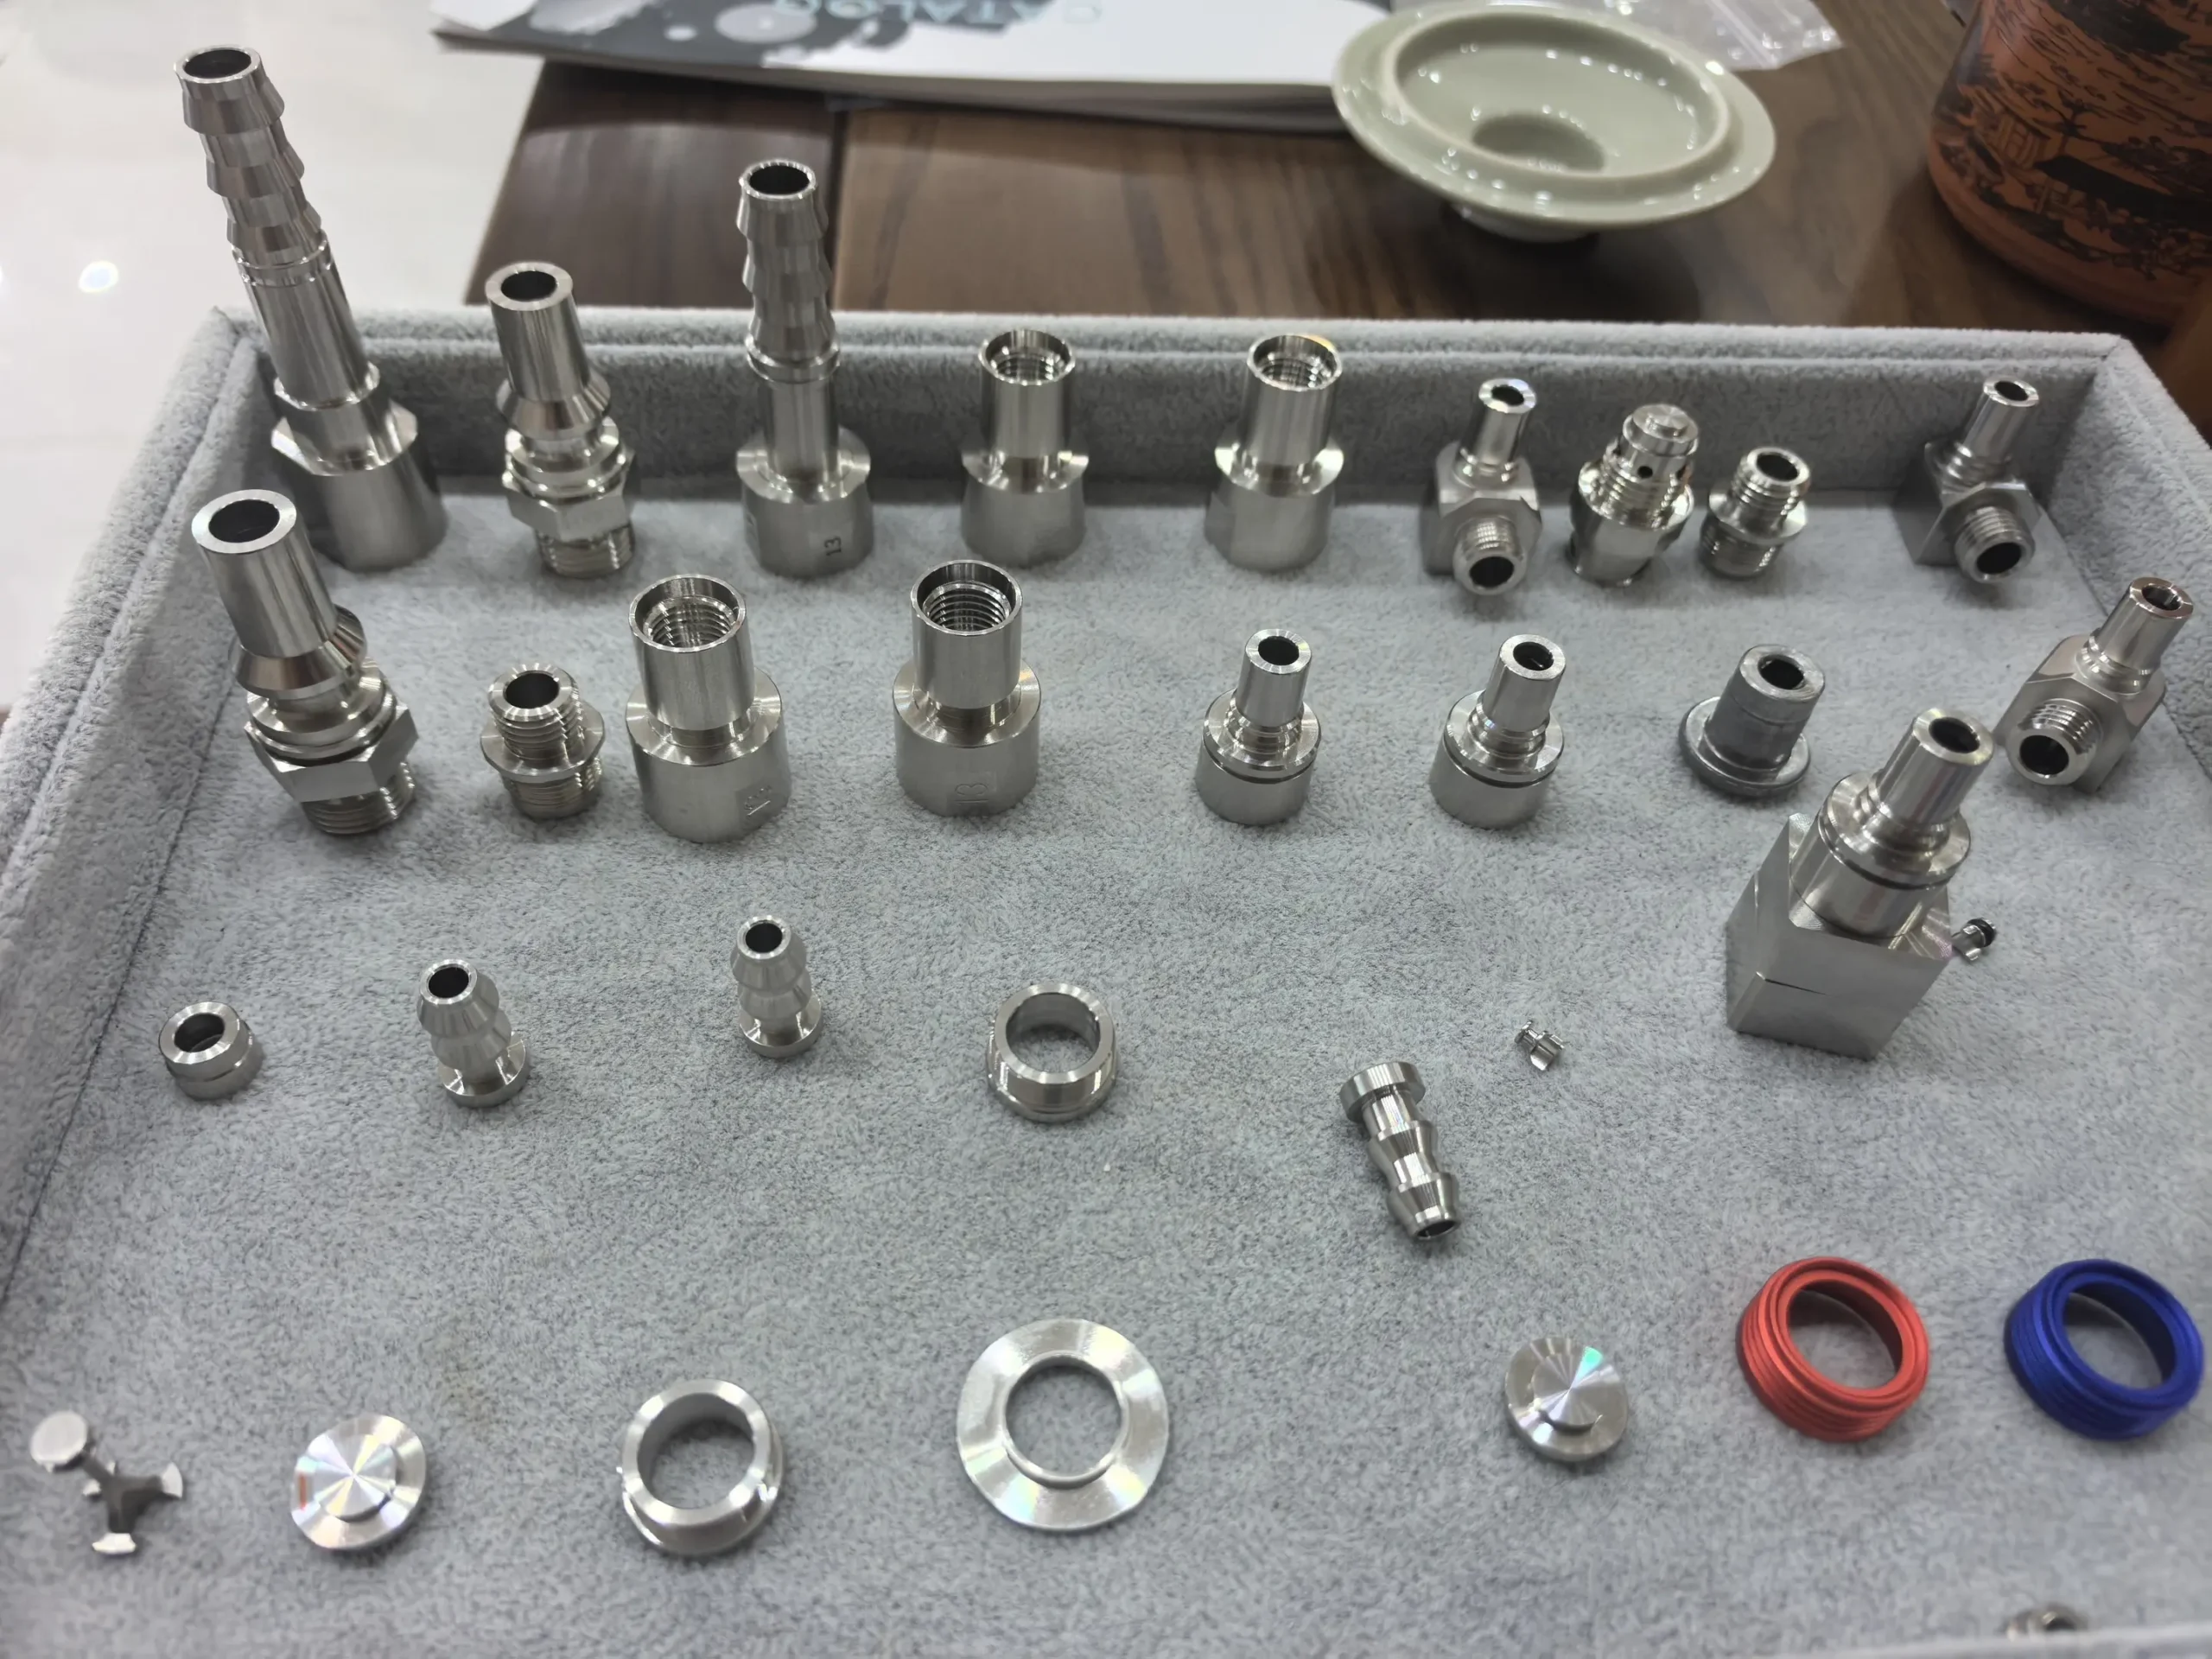
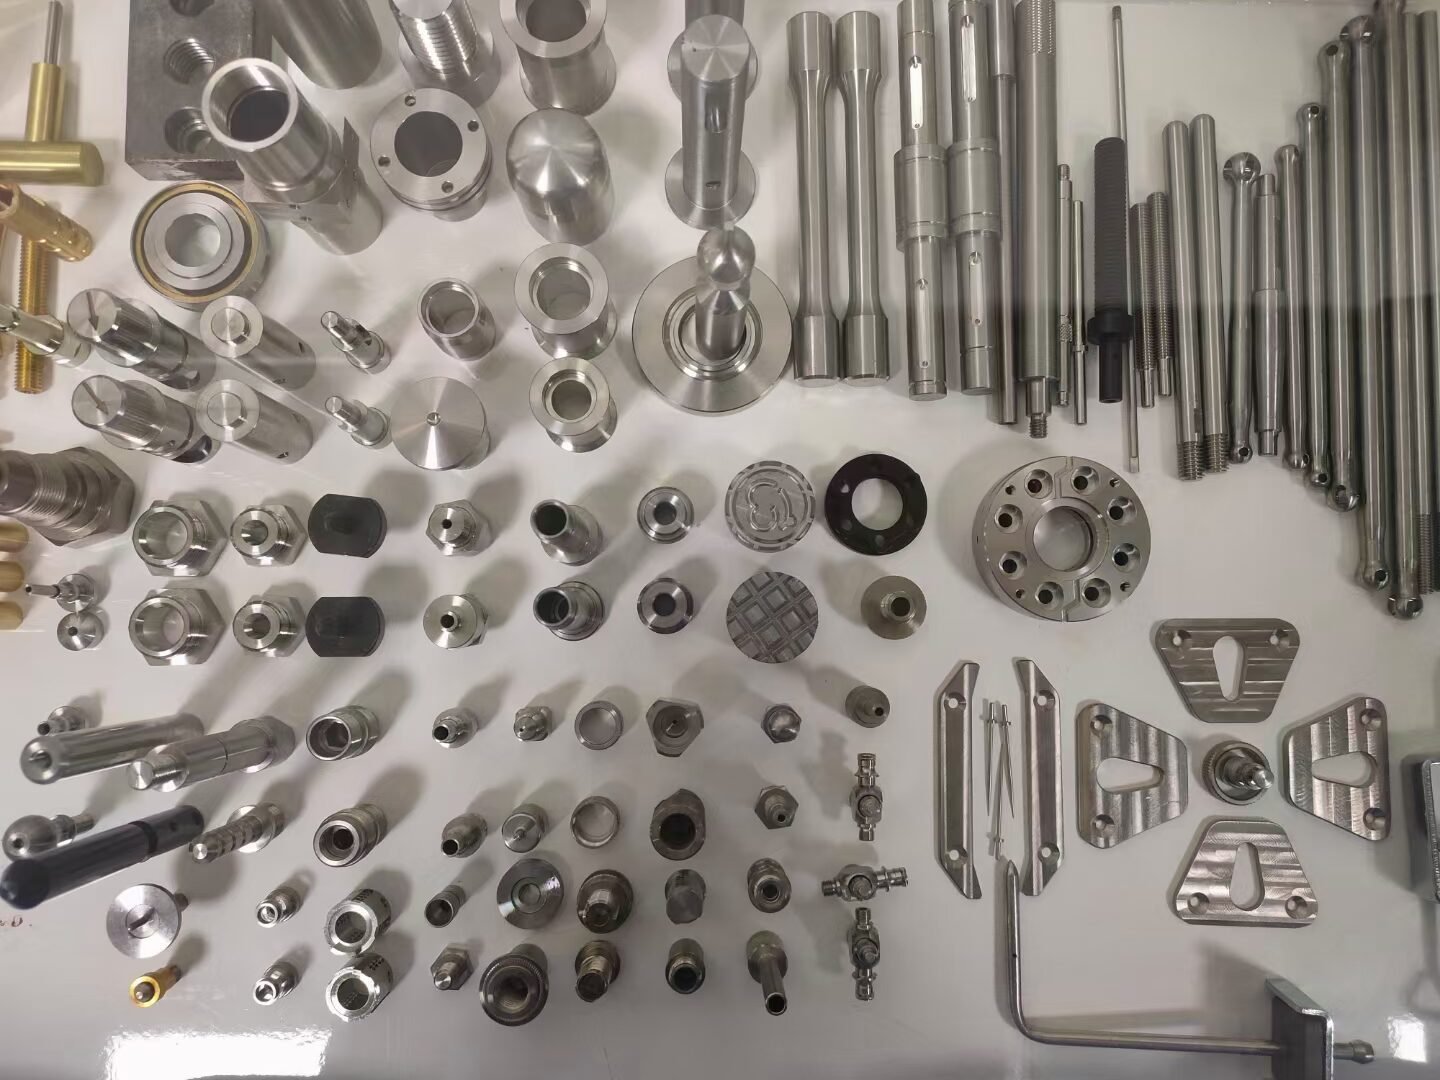
Inside 6CNC: Factory and Precision Parts
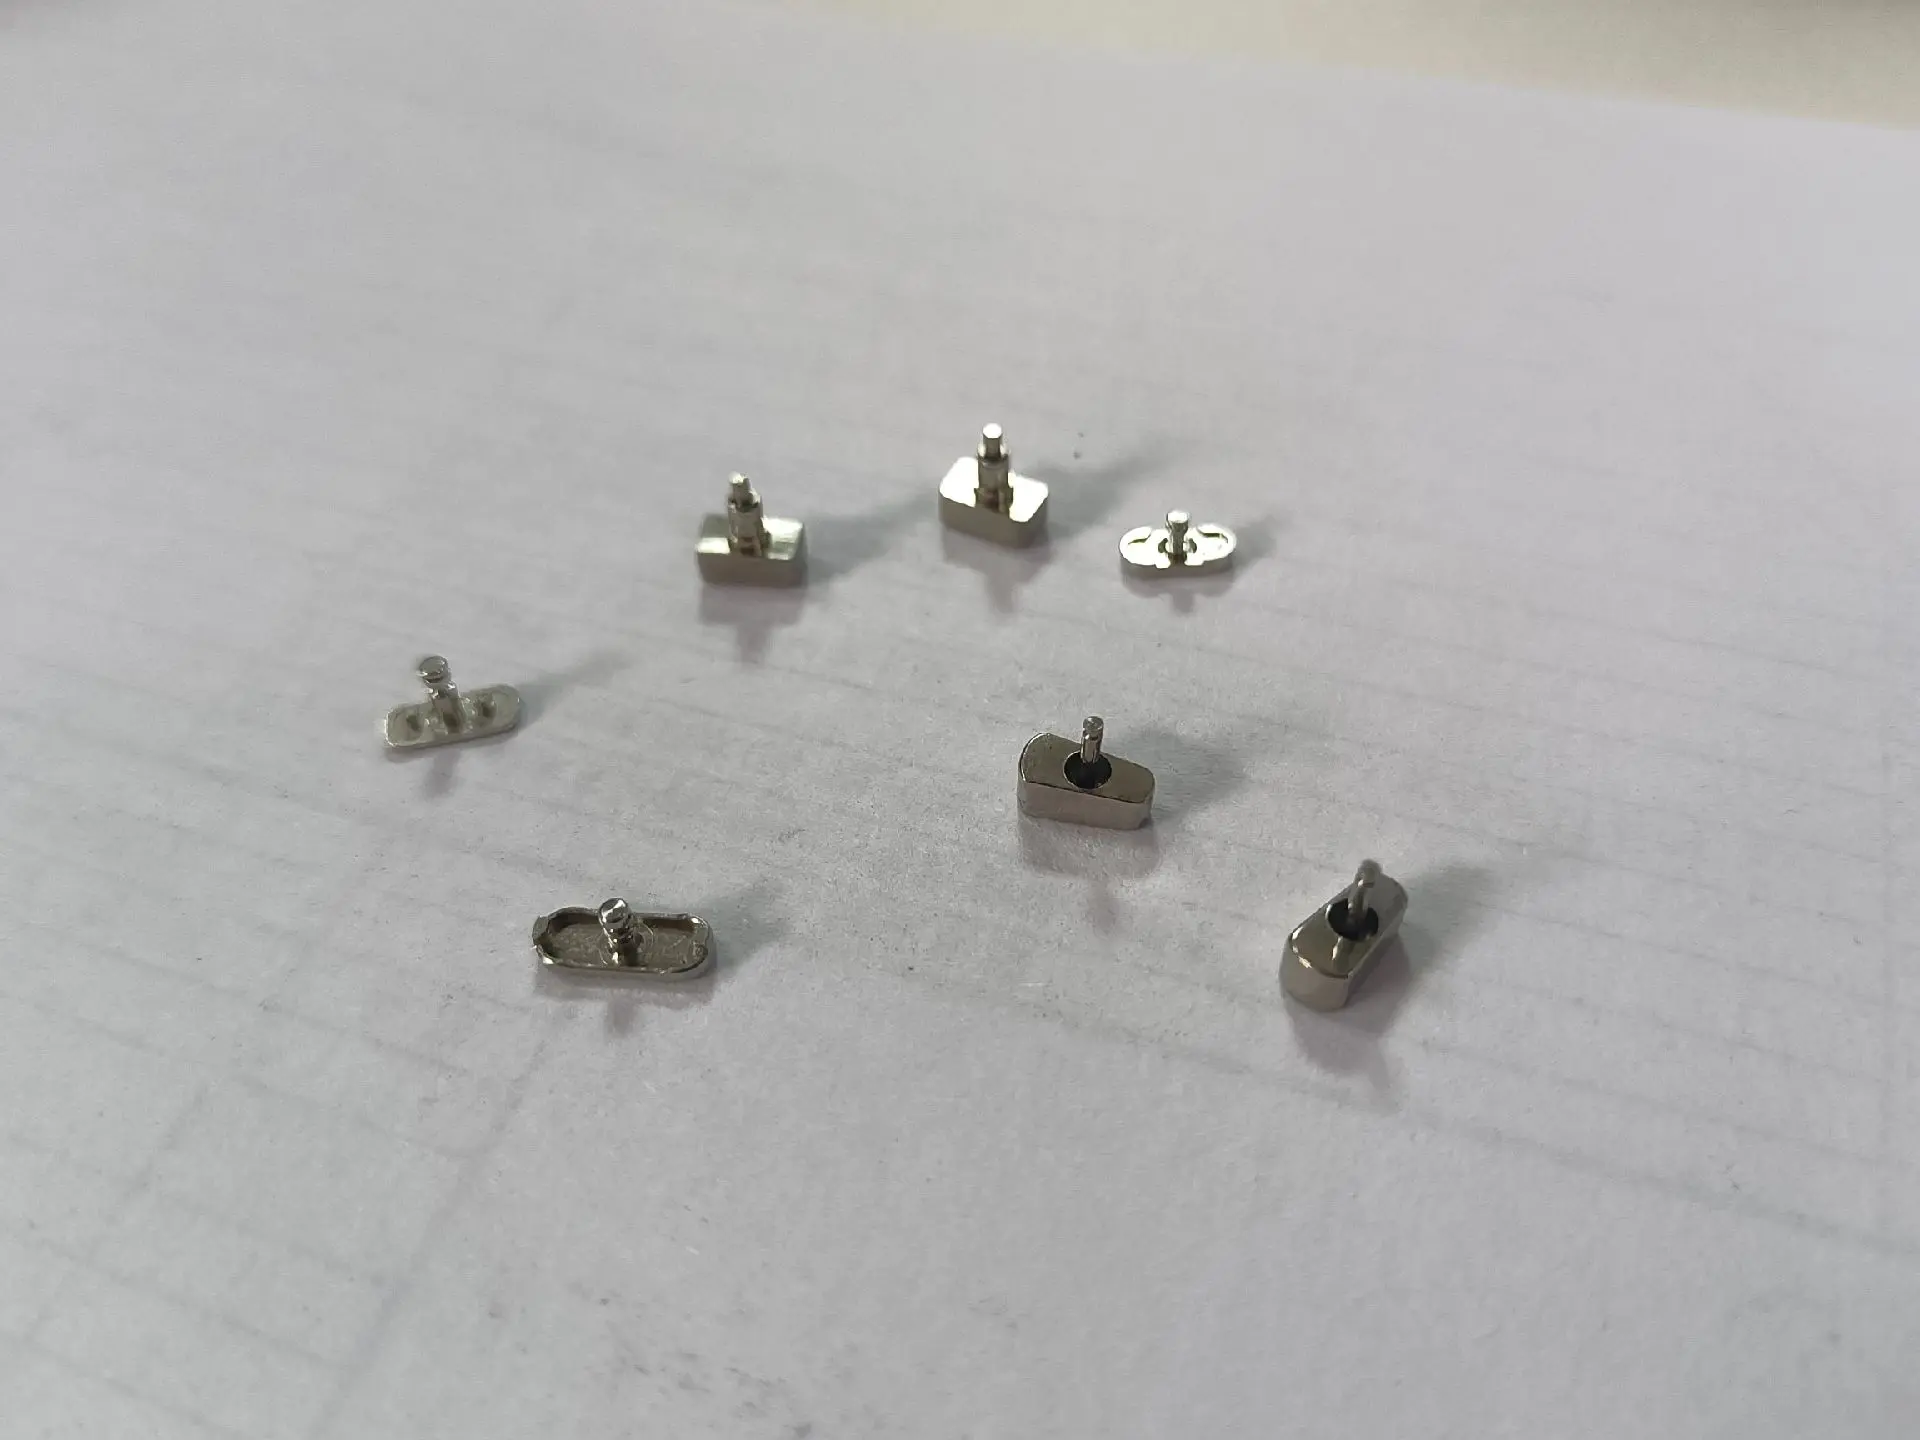
Explore 6CNC’s production lines and precision components. Process selection, machining, inspection and finishing are coordinated around your drawing.
Quality Control for Your Connector
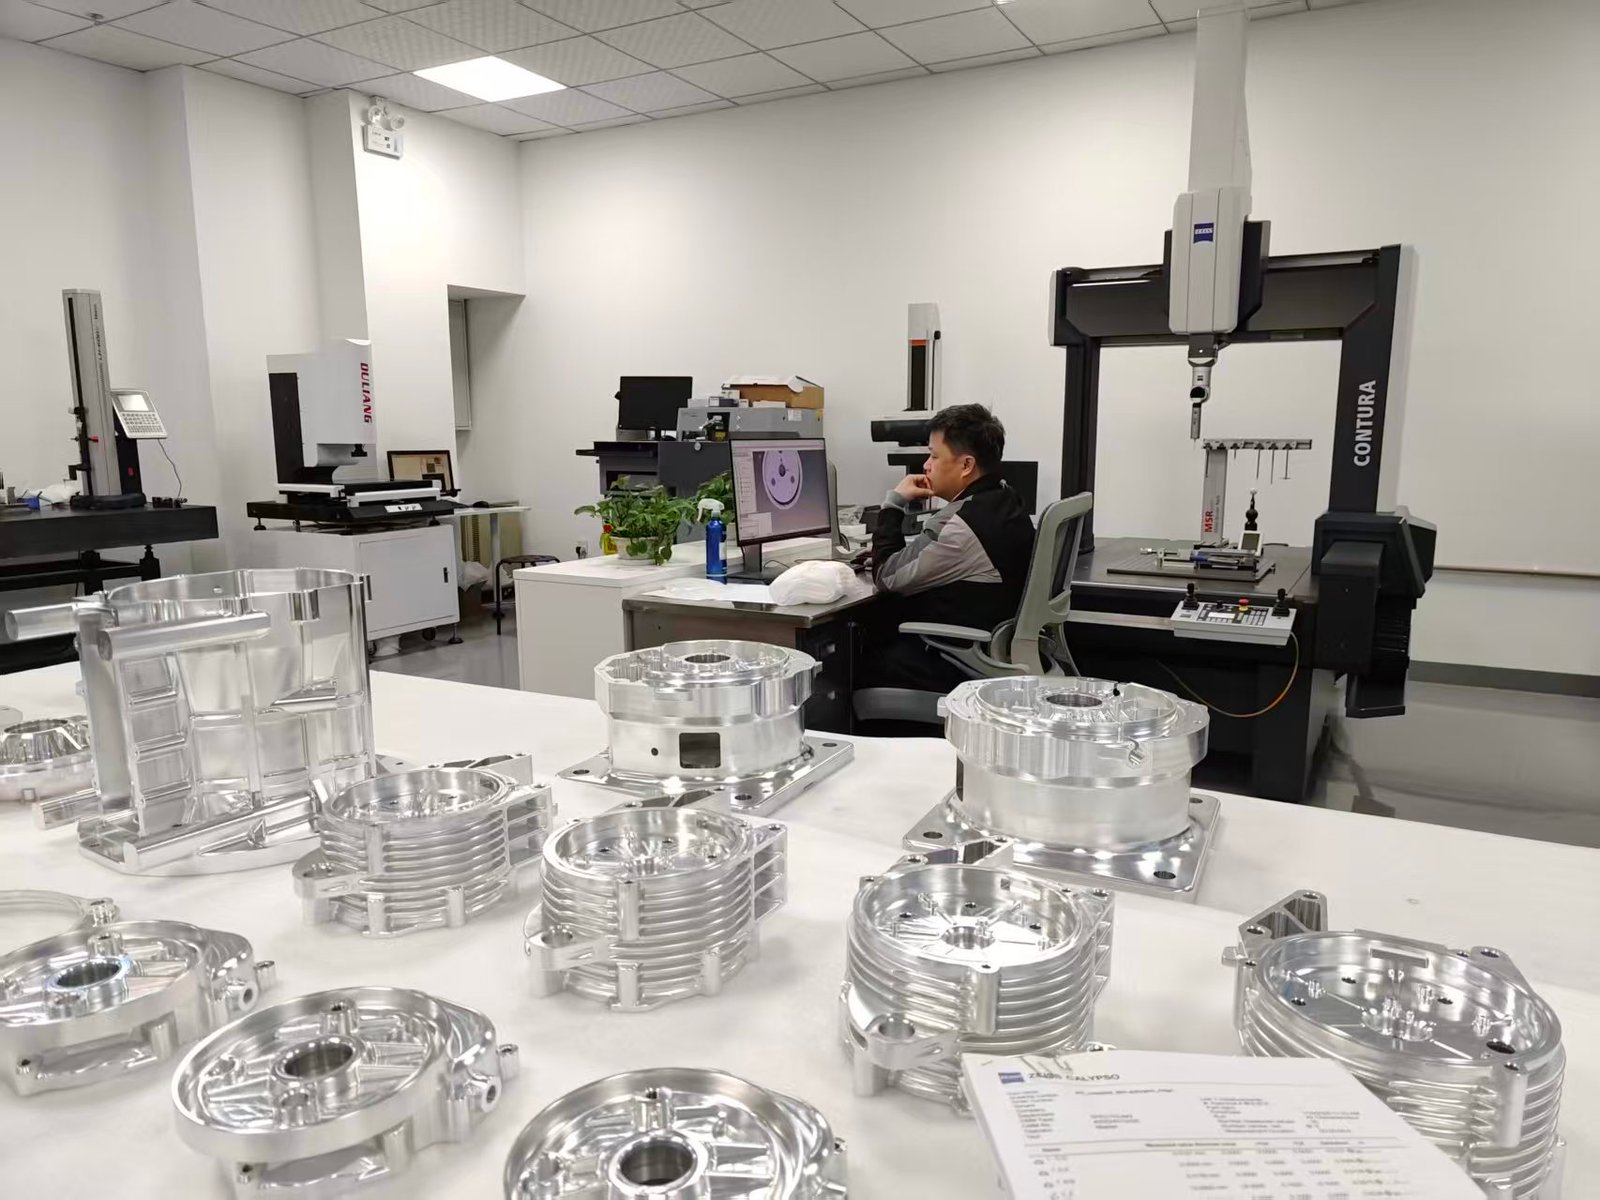
Connector inspection should focus on the features that determine function.
At 6CNC, inspection can include dimensional checks during production and final verification according to drawing requirements.
Our quality team includes 9+ quality engineers, with inspections performed during pre-production, machining, and final inspection.
Inspection equipment
- Coordinate Measuring Machines (CMM)
- 2D optical measurement systems
- Surface roughness testing
- XRF material analysis
- Thread gauges
- Pin gauges
- Plug gauges
- Micrometers
- Calipers
- Height gauges
- Other dedicated inspection tools
Inspection and traceability documents
- First Article Inspection
- Inspection reports
- Certificate of Conformance
- Material certificates
- Process documentation
- PPAP documentation where applicable
- Traceability records
From Prototype to Small-Batch Production
6CNC supports prototypes and small batches of approximately 1–600 pieces, depending on the part and process. Designs can be revised between batches as fit, sealing and assembly requirements are validated.
01
Prototype
02
Functional Testing
03
Design Revision
04
Validation Batch
05
Small-Batch Production
Typical quantities and project fit
Not every connector program requires thousands of parts.
Many specialized products require only:
- Initial prototypes
- 5–20 engineering samples
- 20–100 validation units
- 100–300 pilot-production parts
- Several hundred production units
These quantities can be difficult to source efficiently from suppliers optimized for high-volume production.
6CNC focuses on prototype and small-batch precision manufacturing, supporting connector quantities from approximately 1 to 600 pieces depending on the part and process.
This approach is particularly suitable for:
- New product development
- Engineering validation
- Specialized equipment
- Low-volume industrial systems
- Replacement components
- Product upgrades
- Custom machinery
- Legacy connector replacement
What can change between prototype batches?
A typical connector project may begin with only a few development parts.
During the first production run, engineering teams may discover that:
- A thread needs additional clearance
- A sealing groove requires adjustment
- A cable-entry feature should be repositioned
- A wall section needs more strength
- A mating bore needs tighter control
Instead of immediately committing to high-volume tooling or large production quantities, CNC machining allows the design to be revised between batches.
A project can progress from:
without changing the fundamental manufacturing process.
This is particularly useful for specialized connector designs where product requirements are still evolving.
Applications Across Industries
Connector requirements vary by operating environment, assembly and inspection needs. Select an industry to review its priorities.
Aerospace
Aerospace connector components often require lightweight materials, precise mating geometry, controlled threads, and traceable inspection.
Typical parts include:
- Avionics connector housings
- Circular connector shells
- Sensor connectors
- Cable interface components
- Lightweight aluminum adapters
- Titanium interface components
Small production quantities are common during development, qualification, repair, and specialized aerospace programs.
Medical Devices
Medical equipment may use machined connectors in diagnostic systems, surgical equipment, laboratory devices, fluid systems, and electromechanical assemblies.
Typical priorities include:
- Corrosion-resistant materials
- Smooth cleanable surfaces
- Precision assembly
- Traceability
- Controlled dimensional inspection
6CNC operates quality systems including ISO 9001 and ISO 13485.
Robotics and Automation
Robotic systems contain many compact connector and interface components for sensors, motors, actuators, cameras, cables, pneumatic systems, and end effectors.
These parts often combine tight packaging constraints with multiple mechanical functions.
A small connector housing may need to locate a sensor, protect wiring, provide a mounting interface, and maintain precise alignment—all within a single machined component.
Semiconductor Equipment
Connector and interface components used in semiconductor manufacturing equipment may require precise geometry, clean surfaces, corrosion resistance, and compatibility with vacuum or controlled environments.
Common materials include aluminum, stainless steel, PEEK, and other engineering plastics.
Optical and Precision Instrumentation
Optical systems often depend on mechanical connectors to maintain the position of sensors, lenses, fibers, detectors, and precision assemblies.
In these applications, the connector is not simply joining two parts—it may also establish optical or mechanical alignment.
Frequently Asked Questions
Can you manufacture connectors from an existing sample?
Yes. Where appropriate, connector components can be reproduced from an existing part, drawing, or CAD model. For reverse-engineered parts, critical functional dimensions should be verified before production, especially mating interfaces, threads, sealing features, and assembly relationships.
What is the minimum order quantity for custom CNC connectors?
We can support quantities starting from one prototype. Small-batch production typically ranges from a few pieces to several hundred parts depending on geometry, material, and machining requirements.
Can you machine very small connector components?
Yes. Small connector parts can be manufactured using CNC turning, milling, and precision machining processes. Feasibility depends on feature size, wall thickness, tolerances, tool access, and material.
Can you machine internal and external threads?
Yes. We manufacture metric, unified, pipe, fine-pitch, and other specified internal and external threads. Thread gauges can be used for verification when required.
Can you machine brass electrical connectors?
Yes. Brass is one of the most common materials for machined connector components because of its machinability, conductivity, corrosion resistance, and suitability for plating.
Can you manufacture stainless steel fluid connectors?
Yes. Stainless steel 304, 316/316L, 17-4PH, and other grades can be machined for fluid, hydraulic, pneumatic, instrumentation, and corrosion-resistant connector applications.
Can you provide anodizing or plating after machining?
Yes. We can coordinate anodizing, passivation, nickel plating, zinc plating, polishing, and other finishing processes according to the drawing and application requirements.
Request a Connector Quote
Send your drawing or CAD model with material, quantity, finish, critical tolerances and required delivery date. Our engineering team will review machining feasibility and prepare a quotation.
What to include in your RFQ
- 2D drawing
- STEP or other 3D CAD file
- Material specification
- Quantity
- Surface finish
- Critical tolerances
- Thread specifications
- Inspection requirements
- Required delivery date